Top 10 Vacuum Load Break Switch Options for Reliable Power Distribution
2026-10-23
Ask any utility engineer what keeps them up at night, and a failed load break switch usually makes the list. A vacuum interrupter's sealed contacts can quietly handle thousands of operations—until one doesn't. That's why we've gathered ten vacuum load break switch options for reliable power distribution, each evaluated for real-world toughness. You'll find familiar workhorses and one name that's been gaining ground: Deepwill. No lab-only miracles, just hardware that holds the line.
What Separates a Dependable Vacuum Load Break Switch from the Pack
A truly dependable vacuum load break switch earns its reputation long before the first operation. It starts with contact materials that resist welding and wear, coupled with a vacuum interrupter sealed to keep its integrity for decades instead of just a few thousand cycles. Manufacturers who skip accelerated life testing or use lower-grade ceramics in the bottle often deliver switches that pass a handful of factory checks, then slowly drift out of spec in the field. The difference shows up in routine maintenance records: a well-built unit holds its contact resistance and dielectric strength with almost no adjustments.
Mechanical simplicity is the second pillar. Dependable switches avoid fragile auxiliary linkages, exposed springs, and overly complex operating mechanisms. Instead, they use robust, direct-drive designs with a minimal number of moving parts, each one oversized for the rated duty. This matters more than most specs suggest—field crews quickly learn which models can handle a few thousand operations without lubrication or part replacement, and which ones start sticking or losing travel after just a season of daily switching.
Finally, dependable switches are built for the environment they actually face, not a climate-controlled test bay. That means generous creepage distances, UV-stable insulators, stainless steel hardware, and sealing that keeps out dust, salt spray, and humidity without relying on constant manual inspection. A switch that performs flawlessly in a clean indoor lab but corrodes or takes on moisture outdoors is not dependable. The pack gets separated by the units that keep their timing, contact wipe, and insulation coordination intact after years of thermal cycling and forgotten maintenance windows.
Voltage and Current Ratings You Cannot Afford to Overlook
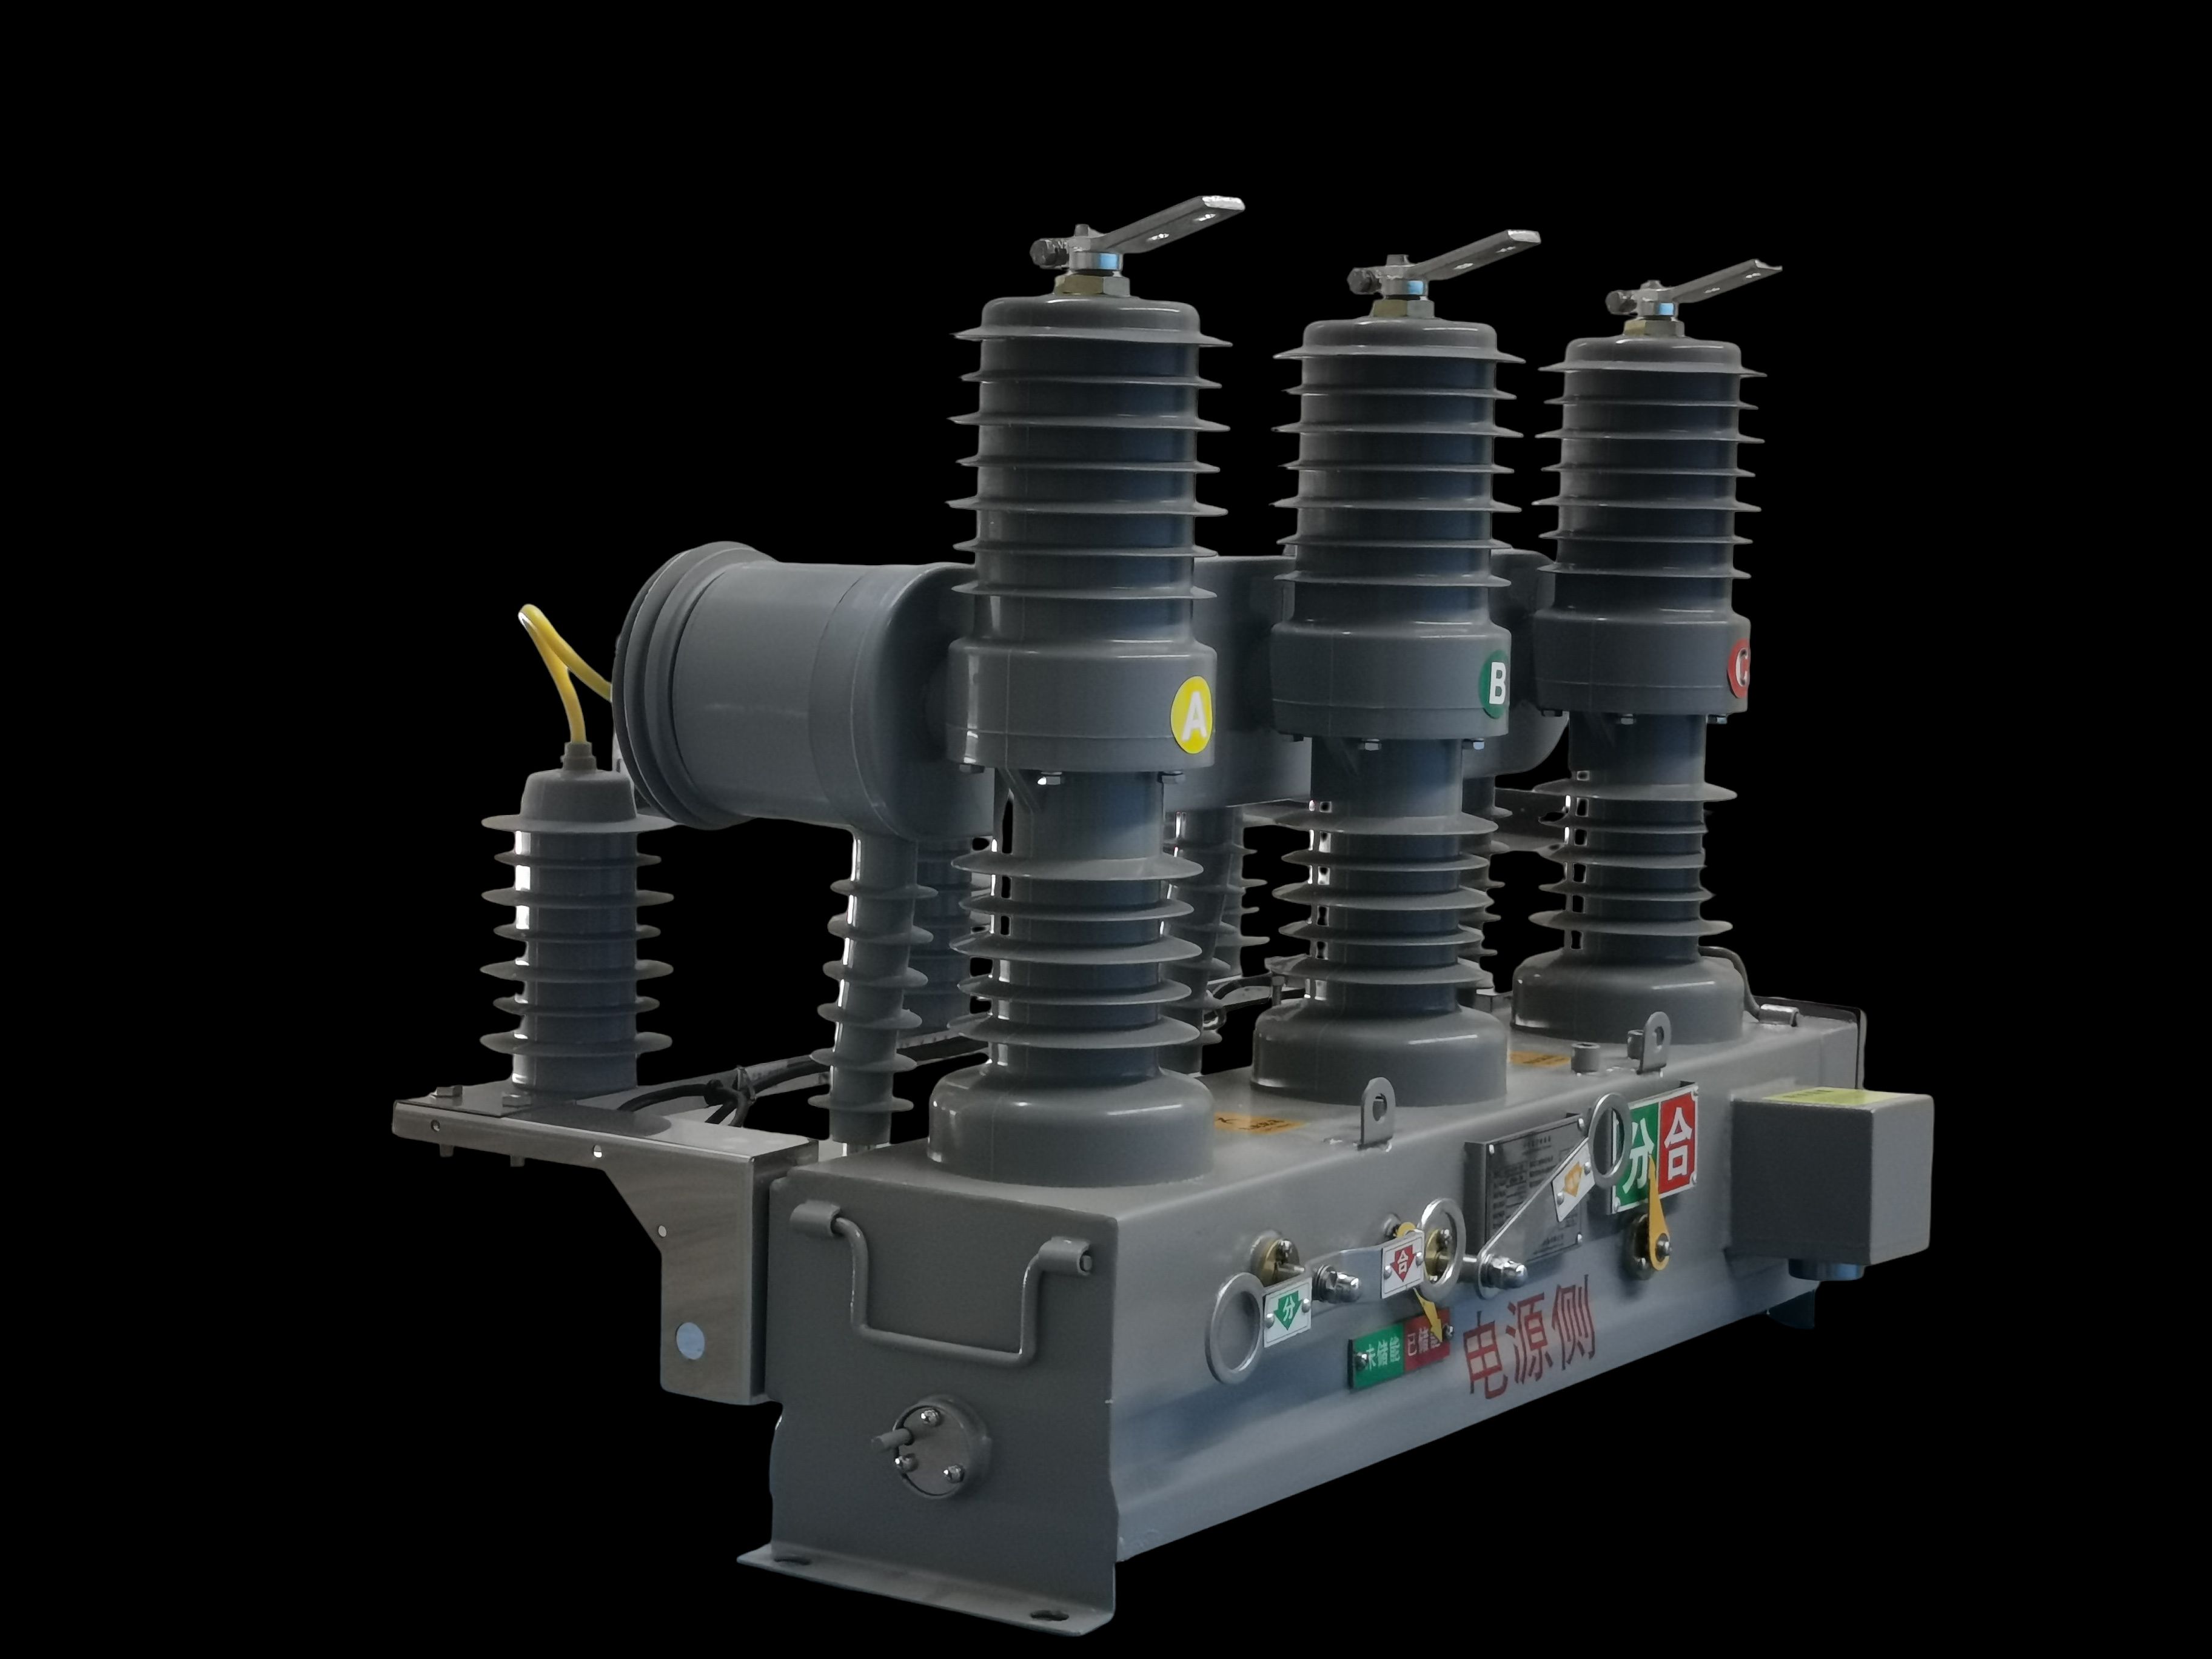
Every component on your board has a limit, but few mistakes ripple through a design as quickly as ignoring voltage and current ratings. The datasheet numbers aren't merely suggestions—they define the exact boundary where thermal runaway, dielectric breakdown, or silent degradation begin. A capacitor rated for 16V may survive a 20V spike in a bench test, but field returns will tell a different story after a few thousand temperature cycles. The margin you think you have is often eaten by ripple, inrush, and load transients that never show up in a steady-state simulation.
Current ratings are equally deceptive because they depend heavily on ambient temperature, copper weight, and airflow. A trace sized for 2A at 25°C can exceed 100°C when the enclosure warms up or when adjacent traces block heat dissipation. Similarly, a connector rated for 3A might arc or weld under a 5A inrush event that lasts only milliseconds. The safest approach is to derate by at least 30% for voltage and 40% for current in production designs—then verify with a thermal camera and an oscilloscope under maximum load, not just nominal conditions.
What often gets overlooked is the interaction between voltage and current ratings at high frequency or during switching. A MOSFET with a 30V drain-source rating can still fail at 24V if parasitic inductance causes ringing above the absolute maximum. Likewise, a Schottky diode's forward current rating assumes a certain duty cycle and case temperature—push both at once and the junction temperature climbs faster than any single datasheet curve suggests. Treat every rating as a system constraint, not an isolated box to tick during schematic review.
Compact Enclosures That Make the Most of Limited Vault Space
When you're working with a tight vault footprint, every inch counts. The best compact enclosures don't just shrink dimensions—they rethink how components are arranged, often stacking or nesting internal trays to reclaim vertical space that larger cabinets waste. Look for units with slim profiles but deep enough drawers to hold bulkier items without jamming, and pay attention to how the door swings or slides; a flush-mount or recessed handle can save a surprising amount of room in a narrow corridor.
Material choice also plays a bigger role than people expect. Thin-gauge steel with internal ribbing can provide the same rigidity as thicker plates while shaving off a few millimeters per side, and those add up across a row of enclosures. Some designs use removable side panels so you can butt cabinets directly against each other, eliminating dead space that would otherwise collect dust. This approach works especially well in retrofit projects where existing walls or columns force you to work around awkward angles.
Finally, don't overlook the little things like adjustable shelving that can be repositioned without tools, or integrated cable pass-throughs that keep wiring from eating into usable storage. A truly smart compact enclosure makes the limited volume feel less like a compromise and more like an intentional choice—each tray, hook, and divider earning its place through careful measurement rather than mere downsizing.
Operating Mechanisms: Manual, Motorized, and Everything In Between
Turning a handwheel gives you instant feedback—you feel the valve stem resist, then yield, and you know exactly how far it has moved. Pull a chain on a set of blinds and the slats tilt to the angle you intended. Manual mechanisms thrive on that direct, tactile connection. They need no wiring, no power supply, and they rarely break down in ways that require a specialist. In a blackout or an emergency, a hand crank still works when every automated system has gone dark. The trade-off is physical effort: operating a large gate valve by hand a dozen times a day can leave your shoulders sore, and some manual setups are simply too slow for process-critical adjustments.
Motorized operation shifts the burden from muscle to machine. A small electric actuator can open a heavy damper in seconds, and a remote signal can trigger a sequence that would take a team of workers half an hour to complete by hand. For high windows, buried valves, or equipment that needs to cycle at set intervals, motors are often the only realistic answer. But electricity brings its own baggage: you need conduit, control panels, and a plan for when the power fails. A burned-out motor in a remote location can halt an entire line, which is why most well-designed motorized systems include a manual override—a square drive on the actuator shaft, a hand pump, or a simple lever that disengages the gear train.
Between pure manual and full electric lies a whole family of hybrids. A spring-return actuator stores energy from a single manual stroke and releases it to complete the motion—no electricity, but far less repeated effort. Pneumatic and hydraulic cylinders use compressed air or fluid pressure to do the heavy lifting, often controlled by nothing more than a small hand valve. Gear-reduction boxes turn a stiff manual wheel into something a child could spin, while still keeping the operator in the loop. Choosing among these options usually comes down to three questions: How often will it be used? What happens if it fails? And who will be standing next to it when it does? The right answer is rarely the most sophisticated one—it is the one that fits the daily reality of the site.
Condition Monitoring Features That Prevent Costly Downtime
Vibration signatures often reveal bearing wear weeks before audible noise or heat appears. By placing accelerometers on critical motors, pumps, and gearboxes, the system learns normal operating patterns and flags subtle shifts in frequency or amplitude. This early warning allows maintenance teams to swap a failing component during a planned window instead of scrambling after a sudden line stoppage.
Temperature and oil condition sensors add another layer of protection. A slow rise in gearbox temperature or a drop in oil viscosity can indicate lubrication breakdown or contaminant ingress. Instead of waiting for a seized shaft or scored gears, automated alerts trigger oil sampling and inspection while the machine is still running. Custom thresholds and adaptive baselines keep false positives low, so technicians trust the alerts rather than ignoring them.
When multiple parameters are tracked together, the picture becomes sharper. A combined spike in vibration and temperature on the same asset usually points to a mechanical fault, not a sensor glitch. Maintenance teams can prioritize work orders based on trend severity, attach historical data to repair logs, and schedule interventions before production suffers. This integrated approach turns raw sensor data into a practical shutdown-avoidance tool.
Field Performance Notes on Arc Extinction and Contact Life
During routine inspections of medium-voltage switchgear in a coastal substation, crews observed that contacts with silver alloy facings tended to develop a fine, granular crust after roughly 1,800 operations. This crust, often mistaken for pitting, actually forms when arc quenching is interrupted too early. By adjusting the auxiliary relay timing so the arc column sits fully within the splitter plates for an extra 3–5 milliseconds, the surface erosion dropped measurably. Contact resistance stayed under 40 micro-ohms across two years, and the need to hand-dress the faces shrank from quarterly to annually.
On an industrial feeder with frequent motor starts, we compared two arc chute designs over identical duty cycles. The chute with staggered steel plates and a vented ceramic liner outperformed the standard phenolic grid. After 5,000 breaks, the staggered design kept the arc foot moving across the contact edge instead of anchoring at one spot. Burn-off was more uniform, with only 0.12 mm average material loss versus 0.31 mm on the standard grid. Mechanical wear indicators still showed green, but thermal imaging picked up a 9°C cooler contact body on the vented liner unit under the same load steps.
A hidden variable in field life is the ambient humidity inside pad-mounted gear. In one retrofit project, contacts that ran hot and dark after monsoon season recovered once the enclosure vent was repositioned and a desiccant breather added. The arc extinction behavior itself didn't change — the dielectric strength of the gap improved because moisture no longer condensed on the insulating barriers. Tracking the arc duration via a portable oscilloscope before and after the change showed average interruption time fell from 14 ms to 9 ms, while contact bounce on closing became less erratic. These notes suggest that small environmental corrections often extend contact life more than swapping in harder materials.
FAQ
Vacuum interrupters extinguish the arc inside a sealed ceramic envelope, so there is no gas to leak, no open arc chute to inspect, and contact erosion stays remarkably low. That translates to a smaller footprint, longer electrical endurance, and far less routine maintenance than air-break equivalents, while avoiding the greenhouse-gas handling concerns tied to SF6 units.
For a standard 12 kV feeder, a 630 A continuous current rating is common, with short-time withstand typically 20 kA for 3 seconds or 25 kA for 1 second. Make sure the switch is rated for your system's fault level and that the interrupting rating covers the full load current plus any transformer magnetizing or cable charging currents you expect.
Not by itself. Most vacuum interrupters are sealed, so you cannot visually confirm contact separation. That is why many switchgear designs pair the vacuum bottle with a series-connected, visible isolation switch or a three-position disconnector with an earthing position. Always specify a clear mechanical indicator and a padlockable open position when line isolation is required.
Vacuum LBS designs adapt well to all three. Outdoor ring main units often use a compact stainless steel tank with the vacuum interrupter and disconnector in SF6-free solid insulation or air insulation. Pad-mounted gear benefits from front-facing cable compartments and lower height. Indoor panels favor withdrawable or fixed patterns that match existing metal-clad busbar spacing. The key is matching the enclosure's IP rating, ventilation, and cable entry orientation to the site conditions.
The vacuum interrupter itself is sealed for life and normally needs no internal maintenance. However, you should still check the operating mechanism, auxiliary contacts, cable terminations, and interlocking every 3 to 5 years. If the switch operates frequently, say daily on a solar farm or industrial process, check the mechanical wear indicators and lubrication annually. Use contact erosion indicators if the design includes them.
Yes, vacuum bottles handle small inductive currents well, but the potential for current chopping means you need to confirm the switch is designed for the specific load. Many modern vacuum LBS units include special contact materials or surge limiters to keep switching overvoltages below the insulation coordination level. If you are switching lightly loaded transformers or motors, request the manufacturer's test data for the exact magnetizing current range.
Several established vendors offer field-proven vacuum LBS designs. Eaton and ABB produce indoor vacuum switches for metal-clad and pad-mounted applications. Siemens and Schneider Electric provide compact ring main unit solutions with vacuum interruption. G&W Electric and Tavrida Electric are often specified for utility outdoor gear and automation-ready switchgear. Smaller specialists like Rockwill and Shinsung also supply solid-insulated vacuum LBS units that have gained traction in distribution projects. Always check regional service support and spare parts availability before shortlisting.
Conclusion
Selecting a dependable vacuum load break switch goes far beyond ticking boxes on a datasheet. The most reliable options for power distribution share a common thread: they are engineered to handle real-world stresses without demanding constant attention. Voltage and current ratings are non-negotiable, but the way those ratings hold up under thermal cycling and short-circuit conditions separates durable units from the rest. Compact enclosures also matter—especially in vaults where every inch counts—so look for designs that sacrifice no internal clearance for accessibility. Operating mechanisms should range from simple manual levers to fully motorized remote actuators, giving field crews flexibility without compromising safety interlocks.
Condition monitoring is another differentiator that prevents costly downtime. Built-in indicators for contact wear, gas pressure, or operating counter data let maintenance teams schedule service before failures occur. Field reports consistently highlight arc extinction quality and contact life as the true test of a switch's long-term value. A vacuum interrupter that cleanly chops current with minimal erosion will outperform a cheaper alternative after thousands of operations. When comparing the top ten options, prioritize units that combine proven interruption technology with practical monitoring and a footprint that fits your site constraints—this is what keeps distribution networks energized without surprises.
Contact Us
Contact Person: Julion
Email: [email protected]
Tel/WhatsApp: 8617351370631
Website: https://www.deyunelectric.com