Specialty Fasteners Factory Crafting High-Performance Custom Bolts and Screws
2026-10-10
Behind every reliable machine, there’s a fastener that never gets the spotlight. At Peak Fasten, we’re not just another specialty fasteners factory—we engineer high-performance custom bolts and screws that hold up when others fail. Whether you’re pushing the limits of aerospace, automotive, or industrial design, off-the-shelf parts won’t cut it. So what really goes into crafting a bolt that can handle extreme stress, vibration, and temperature swings? Let’s take a closer look at the precision, materials, and obsessive quality control behind our custom fastening solutions.
Alloy Choices That Outlast the Environment
Pick the wrong alloy and the environment wins within a few seasons. Coastal salt spray, industrial acid rain, or even the constant damp of a shaded courtyard will chew through standard steel before the first maintenance cycle. The trick isn't just adding chromium or nickel; it's matching the exact corrosive agent to the alloy's passive film behavior. For example, a duplex stainless with 22% chromium and 5% nickel shrugs off chloride pitting that would crater a 304 grade in months, while a simple ferritic grade might outperform both in a dry, high-temperature exhaust stream where oxidation scaling is the real enemy.
Longevity also depends on how the alloy handles micro-environments that designers often ignore. Crevices under bolt heads, weld heat-affected zones, and stagnant water traps create localized chemistry far more aggressive than the bulk atmosphere. A molybdenum-bearing grade like 316L buys years in a marine handrail, but if the fabricator uses a carbon steel brush for cleanup, the embedded iron particles rust first and destroy the surrounding passive layer. Choosing an alloy that outlasts the environment means auditing every joining method, every surface finish, and every shadowed corner where dew lingers after sunrise. Otherwise, you're not specifying a material — you're scheduling a replacement.
Threads Cut to Micron-Level Tolerances
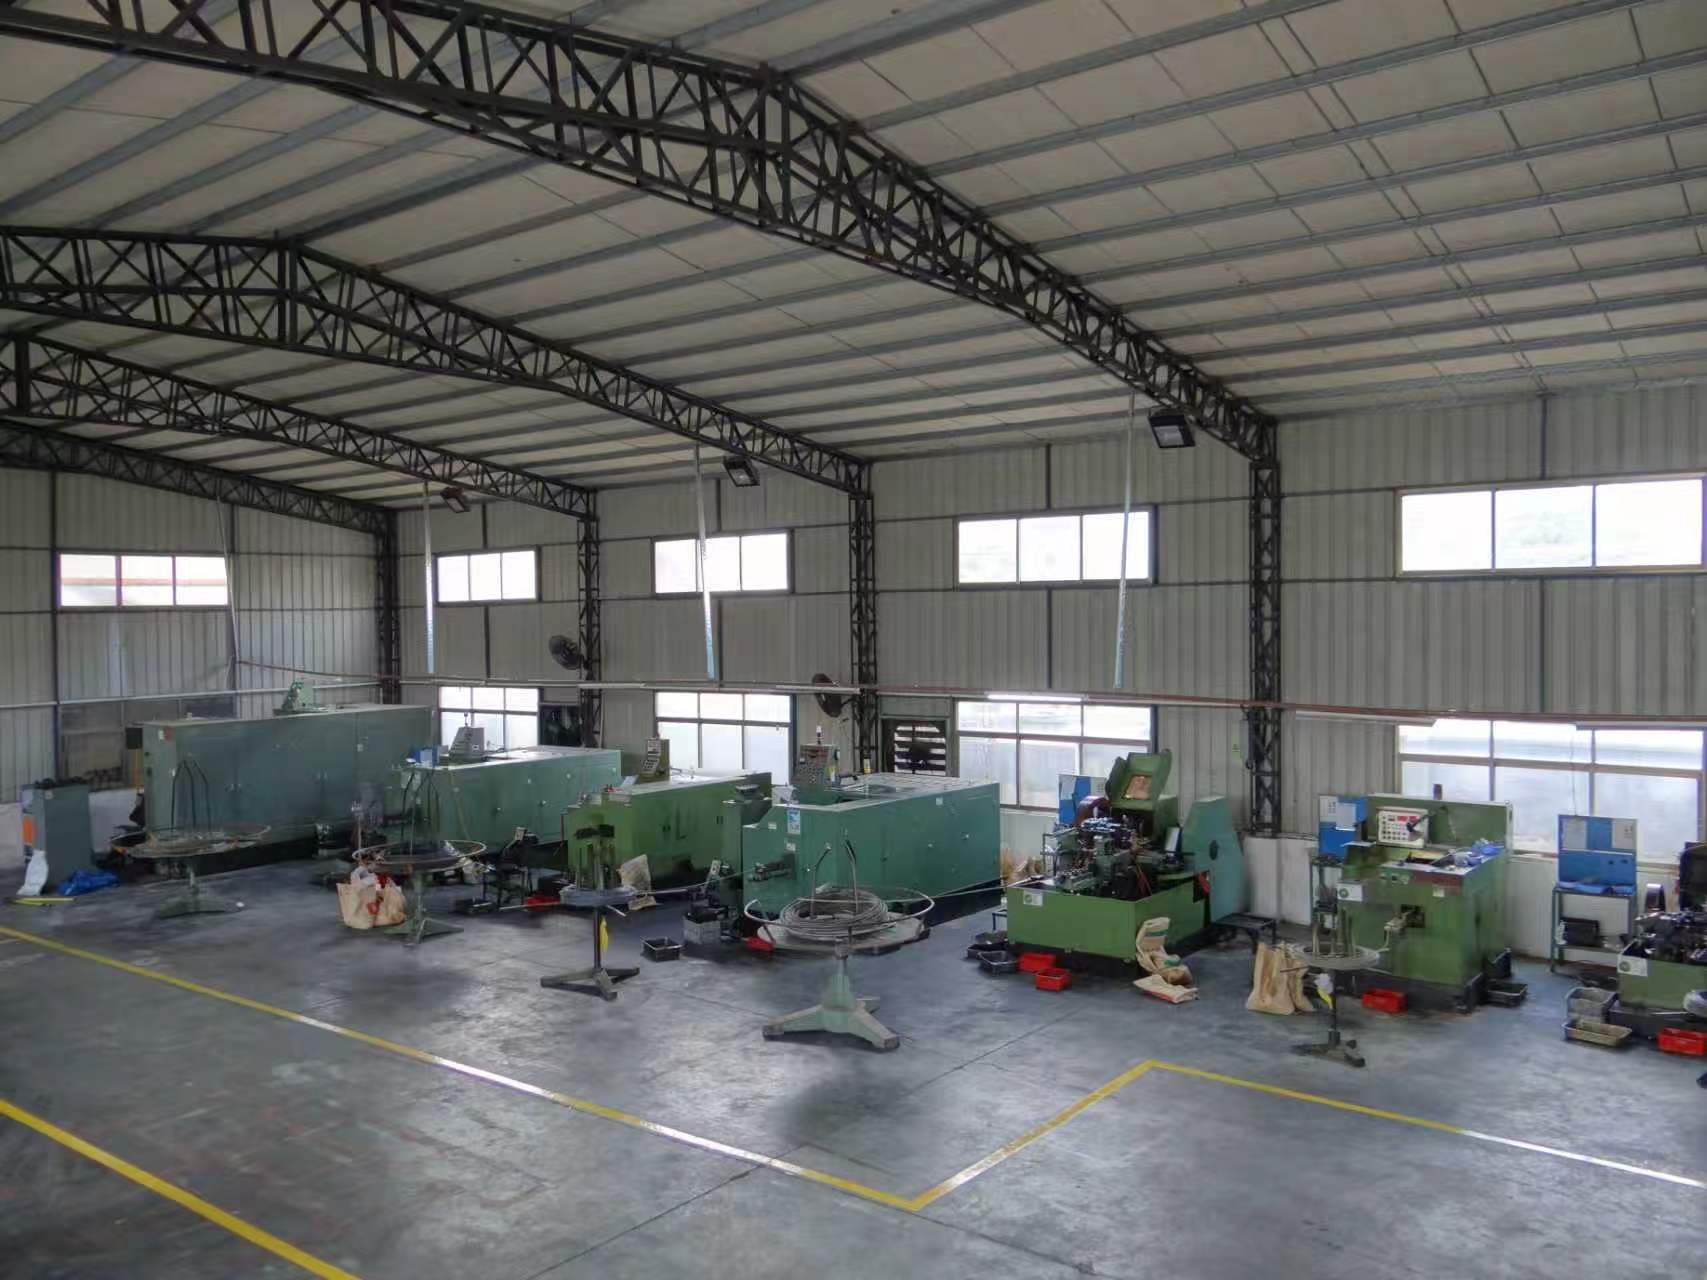
Achieving micron-level thread tolerances is not a matter of simply turning a dial on a standard lathe. It demands a combination of rigid machine construction, temperature-controlled environments, and specialized cutting tools that maintain their geometry over hundreds of passes. The process often involves final grinding or thread whirling after rough machining, removing only a few microns per pass to avoid introducing stress or distortion. Skilled operators read surface finish and pitch diameter measurements in real time, making micro-adjustments that no automated system can fully replicate.
This level of precision translates directly into component reliability. When threads fit within a micron window, there is no room for vibration-induced loosening or uneven load distribution. In fluid systems, a micron-perfect thread prevents micro-leakage that could compromise pressure integrity. For assemblies that undergo thermal cycling, such tightly controlled threads maintain their engagement even as materials expand and contract at different rates, preventing galling or seizure over thousands of duty cycles.
Verification is just as critical as the cutting itself. Optical comparators and coordinate measuring machines are used to profile the thread form, checking not only the pitch diameter but also the root radius and flank angle. Every batch is documented with individual thread records, allowing traceability down to the specific cutting insert and machine setup. This data-driven approach means that a thread cut to micron-level tolerances today can be reproduced identically months later, without relying on tribal knowledge or guesswork.
From Napkin Sketch to Finished Screw
It started as a hasty doodle on a coffee-stained napkin, the kind you draw while half-listening to someone talk about torque values. The first sketch was nonsense, really—a spiral that looked more like a snail than a thread, with arrows pointing to nothing. But that messy line carried the core idea: a screw with a wider minor diameter near the head, just enough to fight off pull-out in soft plastics without needing a separate insert.
Turning that scribble into something machinable meant ruthlessly editing the fantasy. The weird taper got flattened into a stepped shank, the thread pitch bumped from 1.5 mm to 1.25 mm because the prototype shop only had that insert in stock, and the drive socket changed from Torx to hex after the first batch rounded off under a novice's electric drill. We 3D-printed a dozen test pieces, snapped four of them by hand, and learned that the under-head fillet needed a radius nobody had drawn on the napkin.
The finished screw doesn't look much like that original sketch, but it keeps the stubborn promise: bite into cheap MDF or recycled HDPE, hold tight, and strip only when the user does something truly foolish. The final version has a black oxide finish that smells faintly of oil, a dog-point tip that centers itself in a pilot hole, and a head marked with three tiny notches so you can tell it apart from the generic hardware-store junk. That napkin is long gone, but every time I drive one of these into a test block, I remember the exact angle of the original smudge.
Stress-Tested Beyond the Spec Sheet
Spec sheets tell you what a product should survive. They rarely mention what happens when someone accidentally drives over it with a loaded cart, leaves it in a freezing garage for a month, or drops it onto concrete from a ladder for the third time in one afternoon. We decided to find out.
Our test cycle went well past the usual certification checkboxes. We baked units in dry heat, froze them overnight, then immediately ran them at full load. We soaked connectors, vibrated chassis on a shaker table, and simulated years of button presses in a matter of weeks. A few prototypes cracked, one cooling fan gave up, and a power supply threw a fault code we hadn't seen before. Each failure got pulled apart, redesigned, and sent back into the same gauntlet.
What shipped in the end wasn't just a product that passed a lab report. It had survived a punishment tour that most spec sheets don't have language for. That's the difference between 'rated for' and actually ready.
Industry-Grade Bolts for Harsh Jobsites
On a remote bridge rehab in salt spray or a muddy foundation pour, ordinary fasteners give up before the crew does. That’s why these bolts are built around the realities of harsh jobsites—where rain, grit, and heavy impact aren’t exceptions but the daily schedule. The threads are cut with a deeper root radius to resist fatigue cracking, and the heads are designed to take repeated torque from impact wrenches without rounding out. You can feel the difference the first time a bolt seats instead of fighting back.
The coating isn’t just a thin wash that flakes off in the bucket. It’s a bonded, zinc-nickel layer that survives salt fog, chemical overspray, and rough handling, so you don’t waste time chasing rust streaks or seized threads later. We’ve also kept the shank tolerance tight enough to prevent wobble in pre-drilled steel but not so tight that it binds when the alignment is off by a few degrees. That balance means fewer stripped holes and fewer trips back to the supply truck.
Direct Engineer Access, Faster Revisions
When you work with us, you're not handed off to a project manager who then relays your feedback through layers of communication. You talk directly with the engineer building your project. This cuts out the middleman entirely, so your questions get answered on the spot, and your ideas are understood without distortion. Whether you need to tweak a function, adjust a design element, or rethink a feature, the person writing the code is the same person listening to you.
Revisions happen fast because there's no waiting for a ticket to move through a queue. You describe what you want changed, and the engineer can often implement it during the same call. Small adjustments take minutes, not days. Larger changes are scoped immediately so you know exactly what to expect. The back-and-forth feels less like a formal process and more like a working session with someone who genuinely wants to get it right.
This direct access also means fewer misunderstandings. Instead of writing a lengthy brief that might be misinterpreted, you can show the engineer exactly what you mean, share your screen, or sketch out an idea in real time. The result is a final product that matches your vision far more closely, with far less effort spent on correction cycles.
FAQ
Custom bolts and screws built for demanding applications, not generic hardware off the shelf.
Yes, we work with exotic alloys, non-standard thread pitches, and unique geometries. Each order is engineered around your specs rather than forced into a catalog.
Fasteners that survive extreme stress, heat, or corrosion. Every batch comes with testing and traceability, so performance isn't just a claim.
You share drawings or requirements, we review feasibility and produce samples. Full production starts only after you approve the sample.
Automotive, aerospace, energy, heavy equipment—anywhere a failed bolt would be unacceptable.
Yes, low-volume runs are welcome. That's unusual in this industry, but it's part of being a true specialty shop.
Every lot goes through dimensional checks, material verification, and destructive testing when required before it ships.
Standard bolts force your design to compromise. We match the fastener to the load, material, and environment, so the joint works as intended.
Conclusion
When a project hinges on a fastener that has to survive salt spray, thermal cycling, or abrasive dust, off-the-shelf hardware rarely holds up. This shop starts with alloy selections that outlast the environment—think duplex stainless, age-hardened nickel alloys, and titanium grades matched to the exact corrosion and load profile. Threads are then cut, rolled, or ground to micron-level tolerances, so every engagement feels deliberate rather than sloppy. The path from a rough napkin sketch to a finished screw is treated as a collaborative engineering exercise, not a handoff. Dimensions get refined early, material callouts are challenged when a better option exists, and prototypes are machined in small batches to prove the design before a full run.
Before anything leaves the floor, parts are stress-tested beyond what the spec sheet demands. Tensile pulls, fatigue cycling, salt fog exposure, and torque-to-failure runs happen on the actual geometry, not just theoretical coupons. That's why these industry-grade bolts hold up on harsh jobsites—offshore rigs, chemical plants, heavy equipment overhauls—where a failed fastener isn't an inconvenience but a shutdown. Direct engineer access keeps revisions fast; when a thread pitch or under-head radius needs to change, you're not waiting on a sales rep to translate your request. The machinist or metallurgist who can make the call is on the line. It's the difference between buying a part and getting a fastener that actually fits the problem.
Contact Us
Contact Person: Mason Lv
Email: [email protected]
Tel/WhatsApp: +86 13027998452
Website: https://www.peakfastentech.com