Rubber Tire Tread Cooling Production Line Factory Solutions for Efficient Manufacturing
2026-10-16
When rubber tire treads leave the extrusion line at over 100°C, cooling isn't just a step—it's where quality is won or lost. Too slow, and you bottleneck production; too fast, and you risk dimensional drift and surface defects. AUGU AUTOMATION tackles this balancing act with factory solutions engineered for efficient manufacturing, from precision spray systems to modular cooling conveyors. In this blog, we explore how the right tread cooling line design cuts cycle times, stabilizes output, and keeps your plant running at full throttle.
Cooling That Matches Your Extruder’s Pace
Most cooling systems treat every extrusion line the same, but your extruder doesn't run at a constant rhythm. When throughput shifts or melt temperature climbs, a rigid cooling setup either over-cools thin sections or leaves thick profiles soft. The solution is a cooling response that tracks the actual output rate, adjusting airflow or water flow without manual intervention. This keeps the extrudate within its ideal thermal window, so warpage and surface defects stop being a trade-off.
Instead of guessing how much heat to pull, the system reads the extruder's real-time speed and material throughput, then modulates cooling intensity accordingly. At higher line speeds, the cooling fans or chill rolls ramp up; when the extruder slows down for a profile change or start-up, the cooling backs off automatically. Operators no longer need to tweak valves or blower settings with every recipe switch. The result is consistent dimensional stability from the first meter to the last.
This pace-matched approach also helps with energy use. Rather than running cooling at full blast all day, the system only delivers what the extruder demands at that moment. For producers running multiple materials or frequent job changes, this reduces scrap and rework caused by thermal shock or uneven solidification. It turns cooling from a fixed bottleneck into an active partner that adapts like a skilled line operator would.
Uniform Tread Temperature, Every Single Pass
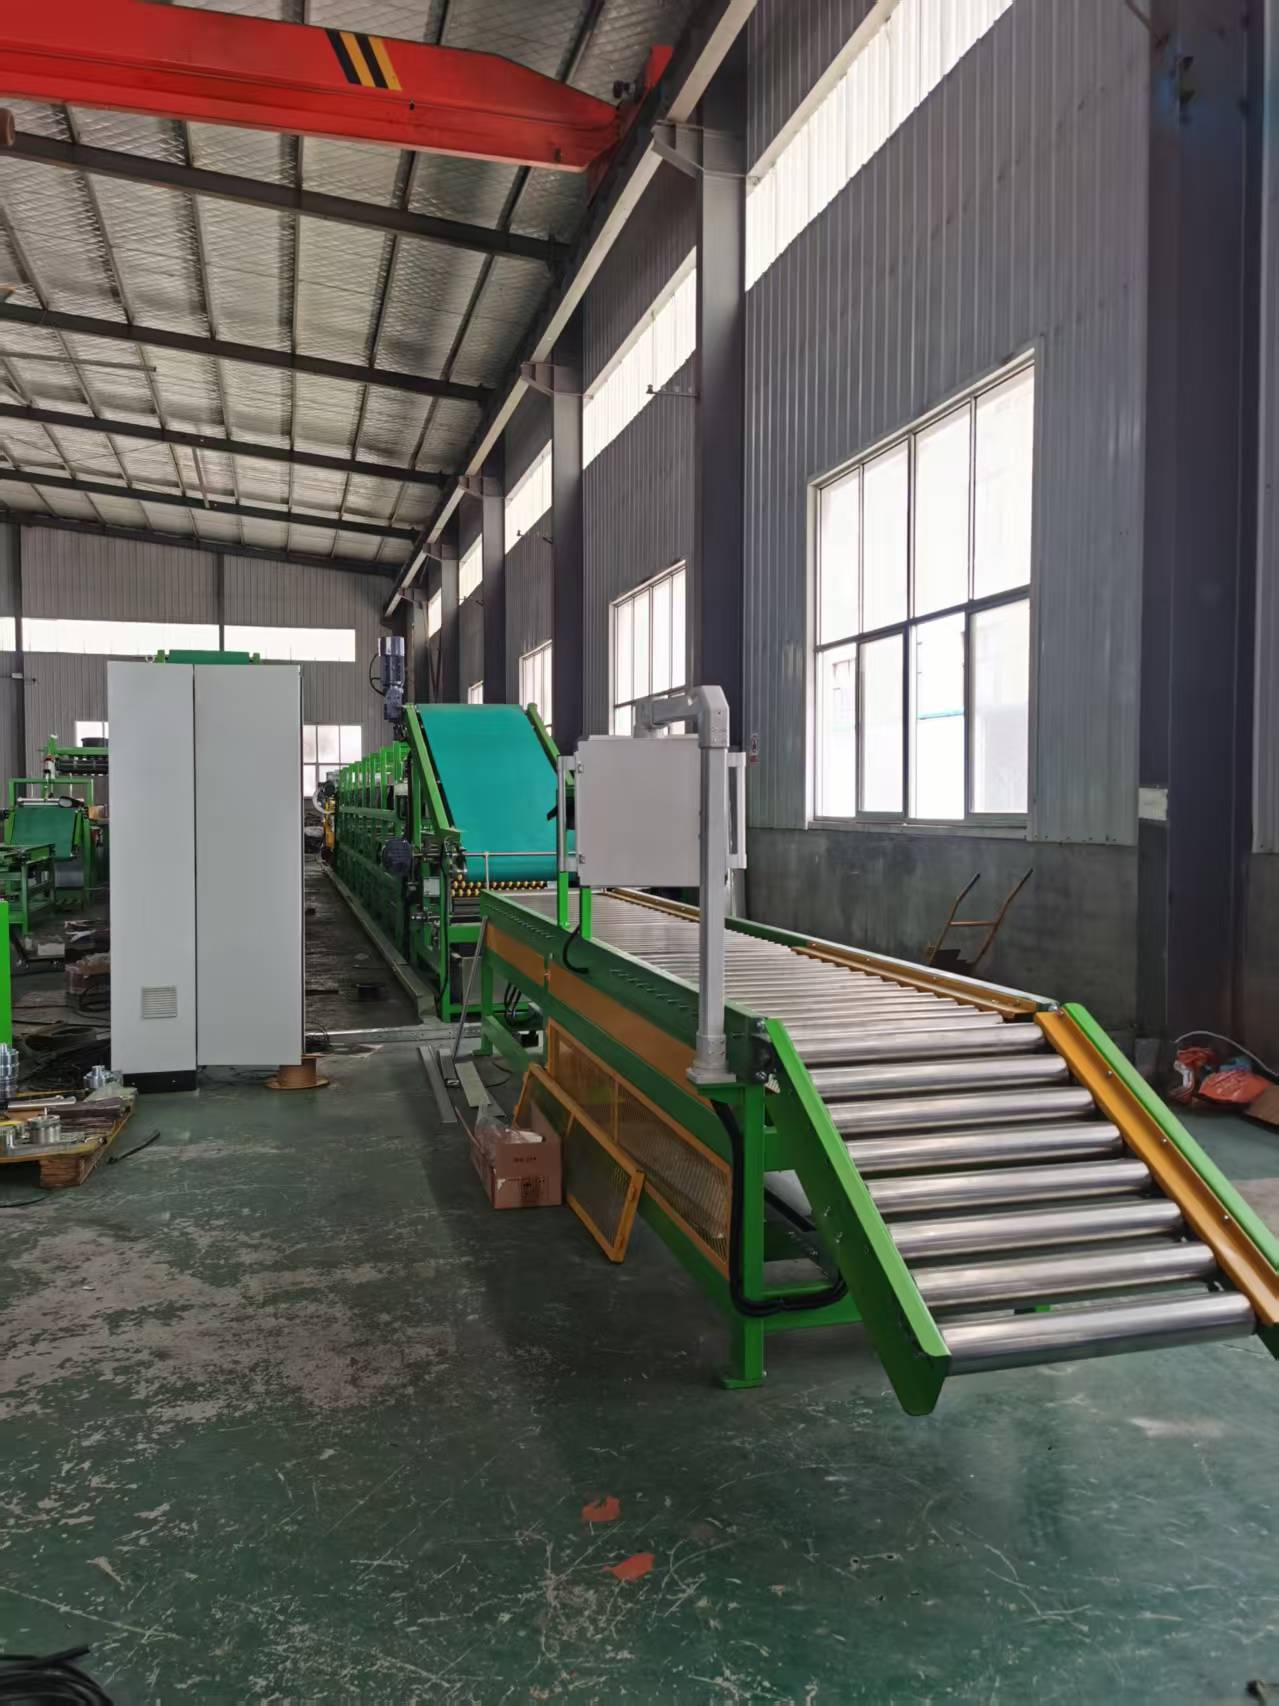
Shaving fifteen seconds off a cure cycle means nothing if shoulder lugs come out undercured while the center rib turns brittle. The principle behind “Uniform Tread Temperature, Every Single Pass” is blunt: every pass through the press has to bring the full tread face to the same thermal set point, not just a rough average.
Most lines still rely on a single thermocouple buried in one spot and assume the rest follows. That assumption breaks down with wider treads, low-profile designs, and compounds that kick fast. By using multiple sensor points and zonal heating control within each cycle, the system smooths out the cold edges and hot crown before they can affect the cure.
You notice the difference in the details—less blistered rubber at the groove tips, fewer tread separations on high-torque drive axles, and less variation in durometer readings across the width. For a retread plant, that translates into lower scrap rates and a casing that can survive another full service life without hidden weak spots.
Less Energy, Same Output—Here’s How
Most operations assume that cutting energy means cutting corners, but the reverse is often true. The quickest wins come from stripping out waste you don't even see: running equipment at partial load, leaving compressors hissing overnight, or heating a whole line just to run one small batch. Tighten those gaps and you can hold output steady while the meter slows down.
People matter as much as machinery. A well-briefed operator who knows exactly when to switch off a pump or adjust a setpoint will save more than any expensive retrofit. Short, practical checklists beat lengthy training manuals, and shutting down idle conveyors, closing oven doors between cycles, or matching motor speed to the actual load often costs nothing to implement.
Then get curious about your energy per unit. A simple sub-meter on a single line can expose spikes you'd never notice on a monthly bill. Fix the leaky steam trap, insulate the forgotten pipe, or recover heat from a compressor room, and you're suddenly making the same product with a smaller draw. No new machines, no bigger budget, just fewer losses between the switch and the shaft.
Line Layouts That Flex With Your Product Mix
A rigid line only works until your product mix shifts. Flexible layouts treat stations as movable pieces, not permanent fixtures. You might roll in a second labeler for a limited run, split a conveyor to feed two pack-out tables, or shift a test bench overnight to handle a high-mix order without a full redesign.
Day to day, the time you save comes from smaller changeover footprints. Crews reposition a few rollers, swap quick-connect tooling, and adjust guide rails instead of rebuilding half the line. That lets you take on short-run orders without wrecking the schedule, while still pushing high-volume products through the same space.
Cutting Cycle Time Without Cutting Corners
Shortening cycle time usually conjures images of rushed work, skipped checks, and brittle outputs. But the most dependable way to move faster is actually quieter: find the wait states that nobody owns. A part sitting in a queue for two days does not need a faster machine; it needs a rule that triggers the next step the moment the previous one is done. Mapping the idle gaps between handoffs often reveals more recoverable time than any amount of overtime ever could.
Speed works better as a design constraint than as deadline pressure. Instead of asking people to 'work quicker,' ask what decision, approval, or format change would let the work flow without stopping. Sometimes the bottleneck is a review step that only catches problems after they have compounded. Moving that check earlier—or replacing it with a short list of non-negotiables—cuts rework and gives teams a faster, safer path through the process.
This approach does not sacrifice quality; it removes the friction that makes quality look slow. A well-run cycle is not about doing less. It is about stopping the stop-and-start rhythm that eats energy and invites mistakes. When the next step is always clear and the handoff is automatic, the timeline shrinks because the work no longer waits for permission to continue.
Why Smart Sensors Beat Guesswork in Cooling
Cooling used to rely on a set schedule and a technician’s hunch. A room that felt warm at noon got extra airflow all afternoon, even after it emptied out. Smart sensors flip that logic by tracking actual heat load, occupancy, and airflow in real time, so the system responds to what’s happening instead of what someone expects to happen.
The difference shows up quickly in buildings with uneven sun exposure or shifting equipment use. One rack of servers may run hot while another idles, but a fixed setpoint can’t tell them apart. Sensors placed near the load detect those pockets of heat and direct cooling only where it’s needed, which cuts compressor runtime and keeps fans from fighting a problem that isn’t there.
There’s also a maintenance angle. When sensors log temperature drift and humidity swings over time, they reveal failing valves, dirty filters, or blocked vents before those issues turn into downtime. That early signal saves more than energy—it prevents the kind of guess-and-check repairs that used to follow every unexplained hot spot.
FAQ
Efficiency comes from combining precise temperature control with smooth material handling. A well-designed line maintains consistent cooling rates across the entire tread width, preventing warping or internal stress. Upgraded spray nozzles, adjustable airflow, and modular conveyor sections also help reduce cycle times without sacrificing product quality.
If the tread cools too quickly or unevenly, it can develop dimensional instability or surface defects. Controlled cooling allows the rubber to stabilize its molecular structure, leading to better wear resistance and adhesion in later building stages. Many factories monitor the cooling bath temperature within a narrow band to ensure repeatable results.
Yes. Most modern lines use adjustable conveyor speeds, interchangeable spray manifolds, and programmable temperature zones. This flexibility lets you switch between passenger car treads and heavy truck treads without lengthy changeovers. Compound-specific cooling recipes can be stored and recalled to avoid guesswork.
The biggest issues tend to be inconsistent water drainage, limited airflow around thick tread sections, and conveyor jams caused by sticky rubber. A practical solution includes self-cleaning spray bars, high-capacity blowers with variable frequency drives, and non-stick belt surfaces. These features keep the line moving and reduce operator intervention.
Closed-loop water recirculation with filtration cuts fresh water use significantly. Variable-speed pumps and blowers only run as hard as needed based on real-time temperature sensors. Some setups also recover heat from the cooling water to preheat other parts of the plant, turning waste into savings.
Daily checks on spray nozzle clogs, belt alignment, and filter cleanliness prevent most unplanned downtime. Weekly calibration of temperature probes and monthly inspection of pump seals and drive chains also pay off. Keeping a small stock of wear parts on-site minimizes disruption when a component fails.
Automated systems continuously adjust cooling parameters based on tread thickness, line speed, and incoming rubber temperature. This removes operator error and ensures each batch matches the approved profile. Data logging also helps trace quality issues back to specific production runs.
Conclusion
In a rubber tire tread plant, the cooling line seldom gets much attention until tread temperatures drift or cycle times creep upward. The real difference shows up when the cooling conveyor moves in lockstep with the extruder, not just at a fixed belt speed. By pairing variable-frequency drives with temperature feedback, each tread pass exits within a narrow band—no hot spots near the sidewalls, no overcooled centers. That same closed-loop control trims energy use because the fans and chillers ramp down when the line runs thinner gauges or slower compounds. Operators stop chasing manual valve adjustments and start trusting repeatable numbers.
Line layout matters more than most factories admit. A modular cooling rack that can be reconfigured for ribbed, lug, or all-season tread patterns removes the bottleneck when product mix shifts between shifts. Instead of waiting for a full batch to finish cooling, staggered zone cooling pulls the first treads off earlier, cutting total cycle time without pushing temperatures below spec. Smart sensors embedded in the spray bars and air knives feed real-time data to a simple dashboard, flagging a clogged nozzle or a drifting chiller before scrap piles up. In the end, the most efficient cooling line is the one that adapts quietly while the rest of the factory keeps running.
Contact Us
Contact Person: Lareina
Email: [email protected]
Tel/WhatsApp: +86 17561696737
Website: https://www.auguauto.com/