High Tenacity Nylon 66 Filament Yarn Factory: A Deep Dive into Manufacturing Excellence
2026-10-04
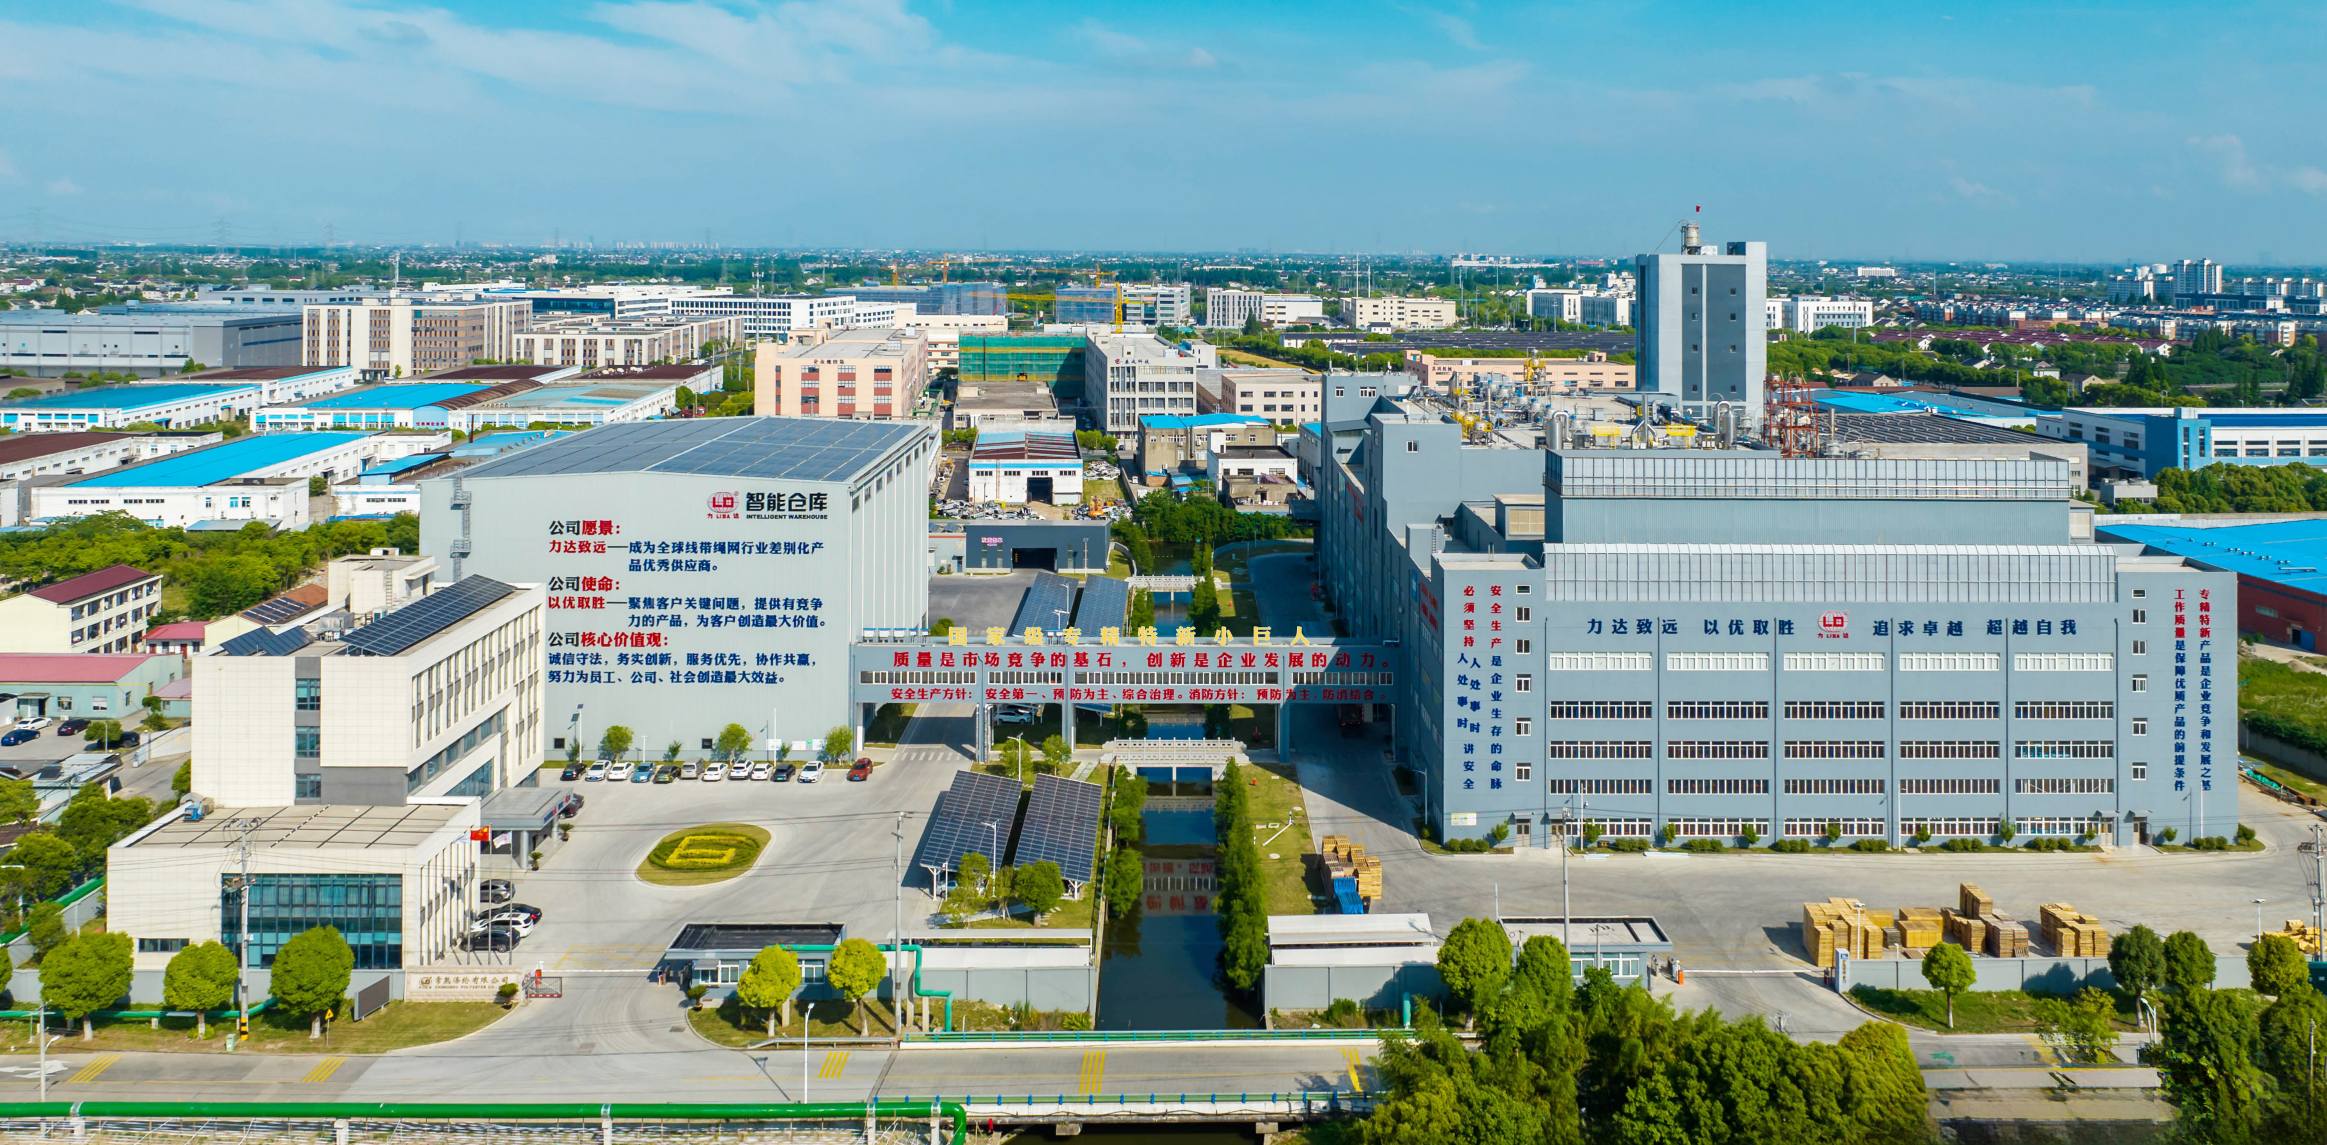
High tenacity nylon 66 filament yarn rarely gets the spotlight, but it's the silent workhorse behind airbags, tire cords, and heavy-duty webbing. What separates a decent factory from a truly excellent one is rarely visible from the outside. At Changshu Polyester, the difference is measured in microns of filament diameter, precise draw ratios, and a testing regime that rejects anything less than flawless. This deep dive walks the production floor and shows how manufacturing excellence is engineered, not assumed.
Why Nylon 66 Starts With Salt: The Chemical Foundation of Tenacity
The path to Nylon 66's toughness begins with a deceptively simple pairing: hexamethylene diamine and adipic acid dissolved together in water. Because the diamine is a base and the diacid is an acid, they neutralize each other on contact, forming a white, crystalline precipitate known as nylon salt. This isn't just a convenience step; it locks in the exact one-to-one molar ratio needed for the subsequent condensation polymerization. Without this precise stoichiometry, chain growth would stall, and the resulting fibers would be short and weak.
Once filtered and dried, the salt is heated under pressure to drive off water and stitch the monomers into long polyamide chains. The amide linkages that form along the backbone are what give Nylon 66 its signature hydrogen-bonding capacity. Those interchain bonds act like tiny zippers, holding neighboring chains in tight alignment. This molecular order translates directly into high tensile strength, abrasion resistance, and the springy recovery that made Nylon 66 a workhorse in everything from tire cord to injection-molded gears.
Molecular Weight Control: The Quiet Battle Inside the Autoclave
Inside every polymer autoclave, a subtle war rages over chain length. Temperature swings, catalyst decay, and monomer feed fluctuations all conspire to shift the average molecular weight away from target. Operators watch viscosity readings like weather reports, knowing that a small drift today becomes a specification failure tomorrow. The quiet battle is rarely visible in control room dashboards, yet it determines whether the resin flows cleanly through a die or tears under stress.
Control strategies often resemble negotiation rather than brute force. A delayed feed adjustment here, a gentle pressure nudge there, and the molecular weight distribution bends back toward spec without shocking the reactor. Too aggressive a correction triggers gel formation or off-spec fines. Experienced engineers learn to read the autoclave's body language: a sluggish heat transfer coefficient, a subtle change in agitator torque, or a whisper of unreacted monomer in the vent line. Each signal hints at the distribution's hidden shape.
What separates consistent producers from everyone else is not better sensors but better mental models. They treat molecular weight as a living response surface, shaped by initiator half-life, solvent viscosity, and even trace oxygen. Small batches of low-molecular-weight polymer can act as chain transfer agents, smoothing out the high end. In the end, the autoclave rewards patience and pattern recognition, not raw control effort.
Extrusion and Quenching: Timing the Melt for Uniform Crystallinity
The window between melt extrusion and the quench bath rarely gets the attention it deserves, yet it is where crystallization either locks in or drifts out of control. Push the extrudate into cooling too soon, and the outer skin freezes while the core still holds excess thermal energy, creating a gradient that shows up later as warpage or uneven mechanical performance. Wait too long, and nucleation starts at scattered points along the melt line, producing a mix of large spherulites and fine-grained regions that no downstream annealing can fully erase.
Operators often rely on fixed line speeds and bath temperatures, but the real lever is the residence time in the air gap. A short, stable air gap—paired with a quench medium that removes heat at a rate matching the polymer's crystallization half-time—keeps the entire cross-section entering the bath at a similar thermal state. This is less about exact temperature readings and more about feel: the melt should still be coherent and slightly elastic when it hits the water, not sagging or showing surface haze.
For semicrystalline grades, a useful trick is to adjust the quench bath temperature upward while slightly increasing line speed. That combination delays the onset of crystallization just long enough for the extrudate to relax internal stresses, then freezes the structure uniformly rather than locking in a skin-core split. The result is a part with consistent crystallinity from surface to center, which translates directly into predictable shrinkage, better fatigue resistance, and fewer rejects in secondary operations.
Drawing Ratios That Decide Between Good and Exceptional Strength
In metal forming, the drawing ratio isn't just a number on a data sheet. It's the quiet variable that separates parts which merely hold up from those that refuse to fail. When you pull a blank through a die, the ratio of initial diameter to final diameter dictates how much the grain structure gets realigned. Push it too far and you're inviting microvoids and surface tears. Hit the sweet spot and the dislocation density climbs in a way that makes the final cross-section surprisingly tough, even after repeated loading. The difference between a standard draw and an optimized one often comes down to a few hundredths in that ratio, yet the performance gap can be dramatic.
Different alloys don't respond to drawing ratios the same way. A soft aluminum might tolerate a more aggressive reduction before cracking, while a high-carbon steel demands a gentler sequence of passes to avoid work hardening that turns brittle. Engineers often keep a running log of how each batch behaves under slight adjustments, because the ideal ratio isn't static—it shifts with tool wear, lubricant temperature, and even the ambient humidity in the shop. Those who treat the ratio as a fixed recipe end up with parts that pass inspection but lack the reserve strength needed for real-world abuse.
Exceptional strength in drawn components rarely comes from exotic materials alone. It comes from refusing to accept the default drawing ratio and instead testing the boundaries of what the material can handle without losing integrity. That might mean splitting a deep draw into two stages with an intermediate anneal, or tweaking the die angle to reduce redundant strain. The result is a part whose grain flow follows the contour so precisely that cracks have no easy path to propagate. Anyone can pull metal through a die. It takes deliberate attention to the ratio to turn a good part into one that outlasts everything else on the assembly line.
Beyond the Datasheet: How We Test for Real-World Fatigue and Abrasion
Datasheets tell you laboratory numbers, but they never tell you what happens after six months of daily use. Our fatigue testing doesn't stop at a fixed cycle count; we replicate the exact loading pattern of a person sitting, standing, and shifting weight repeatedly. We measure how the surface micro-texture changes, where the first signs of loosening appear, and how the material rebounds after sustained pressure. Because real fatigue isn't a single snap—it's the slow accumulation of small failures that eventually become visible.
For abrasion, we avoid the standard flat-surface rub test whenever possible. Instead, we subject each sample to uneven contact, angled scuffs, and repeated impact with common objects like keys, phones, and denim rivets. We then compare the worn area against a reference set under controlled lighting, because what looks fine under bright showroom lights often reveals micro-scratches and color shifts in daylight. This approach shows us not just if it scratches, but how the wear pattern develops and whether it blends naturally or becomes an eyesore.
The result is a testing protocol that prioritizes the messy, variable, and unpredictable nature of actual use. Our engineers log every anomaly, photograph every wear stage, and pull samples at irregular intervals to catch failures that standardized methods miss. We'd rather find the weak point in our lab than have you discover it on your own floor six months in.
Sustainability Inside the Line: Reclaiming Heat, Reducing Scrap, Rethinking Waste
Most factories still treat waste heat as a byproduct to be vented, but that lost thermal energy can offset a surprising share of process demands. Regenerative burners, heat exchangers on exhaust stacks, and closed-loop cooling circuits turn what was once exhaust into preheated combustion air or facility heating. The result is not just lower fuel consumption—it also takes pressure off boilers and reduces the thermal spikes that shorten equipment life.
Scrap reduction tends to be framed as a quality issue, yet the material that never becomes defective product never needs remelting, regrinding, or rework. By tightening tolerances at the point of forming and using real-time dimensional feedback, lines can cut scrap rates by double digits without slowing throughput. That means less raw material ordered, less energy spent on reprocessing, and fewer hidden costs tied to handling rejected parts.
Rethinking waste goes beyond recycling bins. It means questioning whether a process step needs a solvent, a purge gas, or a single-use carrier at all. Some plants have replaced chemical washes with mechanical ablation, switched to returnable dunnage, and found that the "waste" stream from one line can be a feedstock for another. These shifts rarely show up in a single sustainability metric, but they compound into lower disposal fees, cleaner permits, and a shorter material loop.
FAQ
High tenacity nylon 66 starts with a higher molecular weight polymer and a carefully controlled amine end group balance. The extrusion and drawing steps align the polymer chains more completely, reducing amorphous regions and increasing crystalline orientation. This gives the yarn a tensile strength often above 8.5 grams per denier, whereas standard nylon 66 typically sits closer to 5 grams per denier. The result is far better resistance to abrasion, fatigue, and sudden shock loads.
The polymer chips are first dried under vacuum or in a nitrogen atmosphere to bring moisture below 0.02%, since any residual water would cause hydrolytic degradation during melting. The factory also runs intrinsic viscosity tests and gel particle counts on every incoming lot. Only lots that meet a narrow viscosity window and show no detectable black specks or cross-linked gels are released to the silo. This pre-screening prevents the majority of filament breaks and weak points later.
The line uses a single-screw extruder with a static mixer and a spin pack that holds multi-layer filtration screens down to 15 microns. Spinnerets are selected for a low hole count per position to reduce interfiber sticking. Quenching is done with a laminar cross-flow air cabinet, where air temperature and humidity are held within plus or minus 0.5 degrees Celsius and 2 percent RH. This controlled cooling freezes the orientation just enough to survive the next drawing stage without creating skin-core differences.
Drawing is where most of the tenacity develops. The as-spun yarn is first drawn in a hot water or steam bath at 60 to 90 degrees Celsius, then again on heated godets. Total draw ratios usually fall between 4.5 and 6.2, depending on target denier and end-use. Too low a ratio leaves amorphous regions that fail under repeated loading; too high causes fibrillation and broken filaments. The exact ratio is set from a design-of-experiments table built over years of production data.
After drawing, the yarn passes over a set of heated rolls at 210 to 230 degrees Celsius. This annealing step allows some polymer chains to relax while held at constant length, locking in the oriented crystalline structure. Immediately after, the yarn enters a relaxation zone where it is allowed to shrink by 3 to 6 percent. This combination prevents excessive residual shrinkage in the final package and balances tenacity with elongation at break, which is typically kept between 18 and 22 percent for industrial uses.
Every doff is weighed, and a near-infrared analyzer scans the package surface for moisture and finish uniformity. Tensile testing is done on an automatic single-yarn tester that pulls at least 40 samples per pallet, recording tenacity, elongation, and modulus. The data feeds into a statistical process control dashboard that flags any drift in mean tensile strength beyond two standard deviations. Operators can then adjust draw ratio or godet temperature immediately, rather than waiting for the entire batch to finish.
The yarn goes into tire cords, conveyor belts, parachute fabrics, ropes, and heavy-duty webbing. For tire cord, the factory prioritizes fatigue resistance and hot air shrinkage below 5 percent, so it uses a slightly lower draw ratio and a longer heat-setting dwell. For ropes and slings, elongation is allowed to rise a bit while keeping tenacity above 9 grams per denier. Each product family has a separate card of target values for denier, filament count, finish type, and package density, so the same base line can switch between specs with minimal downtime.
Conclusion
The production of high tenacity nylon 66 filament yarn begins well before the spinneret, with the nylon salt formed from hexamethylene diamine and adipic acid. This salt is the chemical backbone that sets the stage for tenacity; its purity and stoichiometry directly influence how the polymer chains will later align. Inside the autoclave, molecular weight control is a quiet but decisive battle. Operators manage temperature ramps, pressure release, and residence time to push the polymerization toward a high, uniform molecular weight without gel formation or degradation. Once the melt leaves the reactor, extrusion and quenching become a matter of timing. The melt must pass through precisely engineered spinnerets and then be cooled at a rate that encourages uniform crystallinity across each filament, because uneven cooling creates weak spots that no downstream process can fully repair.
Drawing is where good yarn becomes exceptional. The draw ratio—often between 4:1 and 6:1 for high tenacity grades—stretches the polymer chains into alignment, dramatically raising tensile strength and modulus. But datasheets alone do not tell the whole story. Our factory runs fatigue tests that cycle samples thousands of times under load, and abrasion tests that simulate years of rubbing against guides and fabrics, because real-world failure rarely looks like a simple tensile break. Sustainability is woven into the same line: heat from the quench air and draw rolls is reclaimed to preheat incoming polymer or building water, edge trim and off-spec filament are regranulated rather than discarded, and water used in finishing is filtered and returned to the process. The result is a manufacturing system where chemical precision, thermal control, mechanical drawing, rigorous testing, and resource recovery operate as one continuous discipline rather than separate departments.
Contact Us
Contact Person: CONNIE
Email: [email protected]
Tel/WhatsApp: 86-0512-53671634
Website: https://www.lida-yarn.com/