Food Grade Oil-Free Air Compressor Supplier Selection Tips for Food Processing Facilities
2026-09-26
Compressed air in food processing is more than a utility—it's a potential contamination vector. One misstep in oil-free air supply, filtration, or condensate management can trigger product holds, audit failures, or worse. Yet with so many vendors claiming 'food-grade' and 'oil-free,' separating real compliance from marketing is hard. That's why we've compiled these food-grade oil-free air compressor supplier selection tips for food processing facilities: what certifications to verify, how to evaluate air treatment and dew point stability, and which service commitments actually protect uptime. And if you're ready to move beyond generic options, Seize Air delivers systems and support purpose-built for food safety environments.
Pin down what “oil-free” actually means for your audit trail
A vague promise of “oil-free” is where audit trails go to die. If your documentation doesn’t define the term, every later review becomes a game of guesswork. Are you excluding mineral oil but allowing plant-derived squalane? Does an ingredient that contains trace esters count? Without spelling out the exact chemical boundaries and the test method used to verify them, the audit trail cannot show why a particular batch was accepted or rejected.
Pin the term to measurable criteria before the first record is filed. State whether “oil-free” means zero lipids above a detection limit, absence of specific CAS numbers, or simply no ingredients with “oil” in the common name. Then link that definition to the raw data: supplier statements, GC-MS results, or formulation software flags. When an auditor pulls a random entry, the chain from definition to decision should be obvious, not inferred. A tighter definition turns “oil-free” from a marketing phrase into a checkable claim.
Match air purity to the food contact surface, not the whole plant
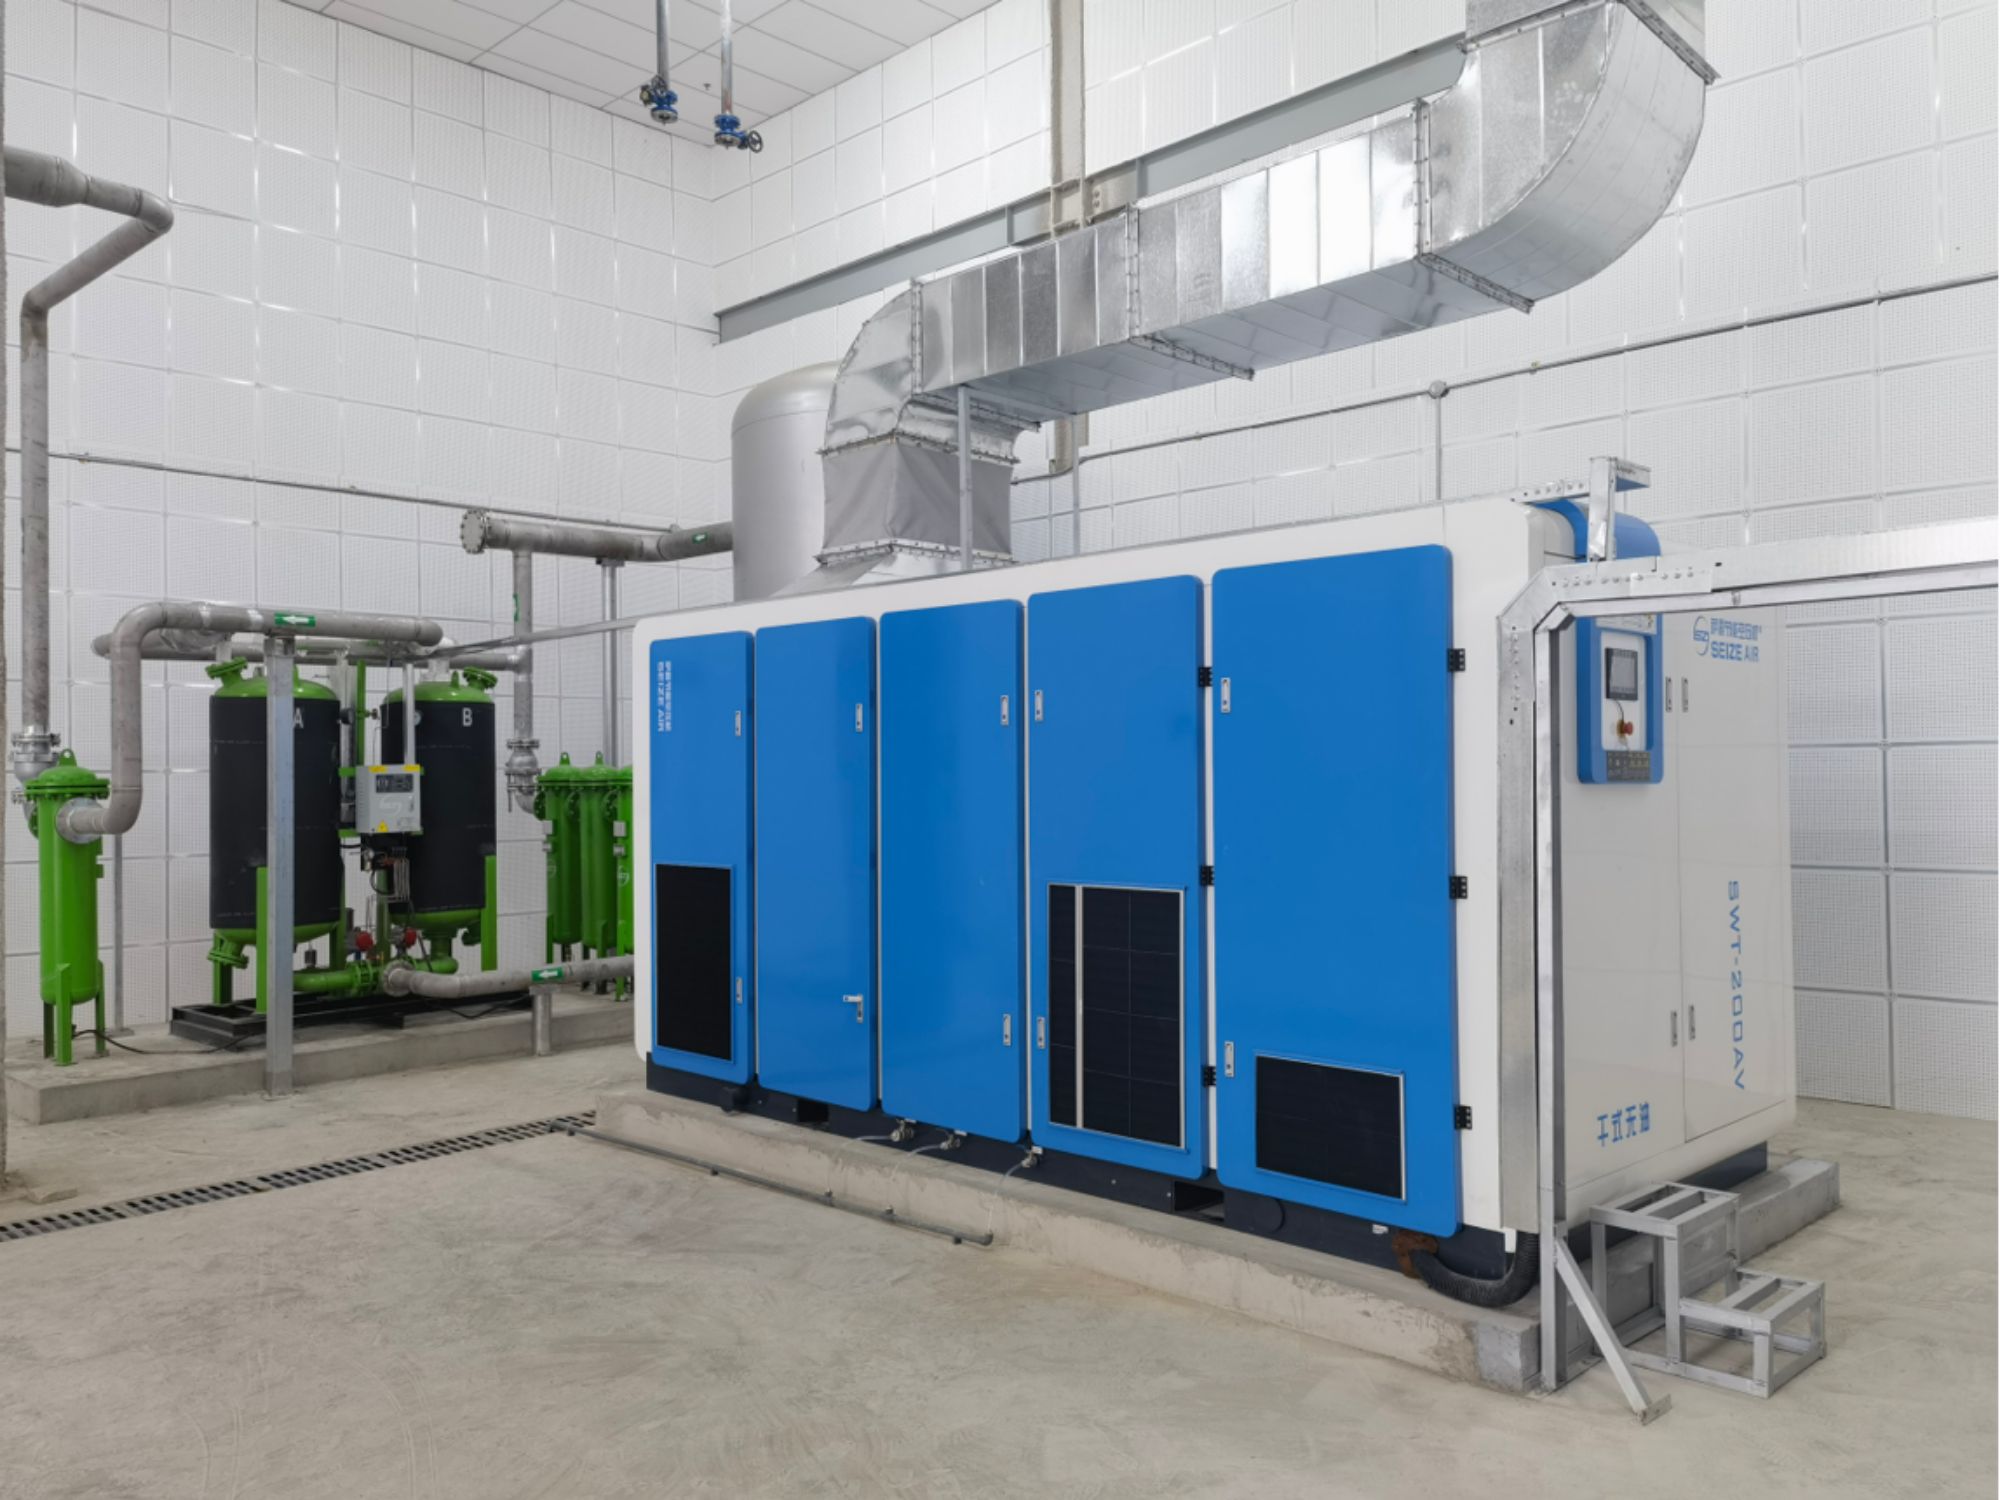
Many food safety plans treat clean air as a plant-wide constant, but that overspends and misses risk gradients. Air purity should follow the surface: zones where product is exposed, like conveyor belts, filling heads, and open mixing vessels, need stricter microbial and particle control than storage hallways or packaging areas where food is already sealed. Shifting from whole-plant to surface-focused monitoring lets teams put HEPA filtration and positive pressure where contamination actually lands.
In practice, map the airflow pathways that touch contact surfaces. A dairy filler might need ISO Class 7 air directly above open cups, while the surrounding room can run at ISO Class 8 or 9 without added risk. Use settle plates and particle counters at the product line, not just in the center of the room. That gives a truer picture of what settles on food, and it avoids wasting energy on overcooling, overfiltering, or pressurizing empty corners.
This approach also simplifies audits and sanitation. Instead of documenting plant air as one vague parameter, you record purity at each critical surface: slicing blades, depositing nozzles, conveyor gaps. When a deviation happens, root cause is localized—maybe a torn filter hood above the depositor, not a whole HVAC overhaul. That both cuts costs and strengthens the defense of actual product contact points.
Ask for references from facilities with similar processing conditions
Talking to operations that run under nearly identical temperatures, pressures, or sanitation cycles often reveals more than any data sheet. A quick call to a plant manager who has already dealt with the same bottlenecks can highlight wear points, maintenance intervals, and unexpected downtime triggers that never appear in vendor brochures.
It helps to ask not only what worked, but what they had to modify after installation. One facility might mention that a particular pump required custom seals after three months, while another could share how they adjusted line speed to avoid frequent jams. These practical details, gathered from a handful of honest references, usually give a clearer picture of long-term reliability than controlled demos or lab results.
Look beyond the compressor at dryers, filters, and condensate management
Many facilities focus almost entirely on the compressor itself, but the equipment installed downstream often determines the actual air quality and long-term operating cost. Dryers, filters, and condensate management are not peripheral add-ons; they directly affect tool wear, product rejects, and how often the maintenance team has to intervene. A well-chosen treatment chain can extend the life of the compressor and every pneumatic device connected to it.
For dryers, the choice between refrigerated and desiccant types comes down to the required dew point. A refrigerated dryer handles general plant air without much fuss, while desiccant dryers become necessary for instrument air or processes that cannot tolerate any trace of moisture. Filters need to be staged properly as well: a general-purpose particulate filter first, then a coalescing filter, and sometimes an activated carbon unit for oil vapor removal. Skipping a stage or using the wrong micron rating usually creates excess pressure drop and shortens element life.
Condensate management tends to be ignored until a drain fails. Timed electric drains are simple but can waste compressed air, whereas zero-loss drains save energy but need periodic inspection to avoid clogging. The collected condensate is often contaminated with oil, so it must pass through an oil-water separator before disposal. Getting this part right keeps the entire system efficient, not just the compressor itself.
Press for realistic maintenance intervals in a food environment
When you operate in a food environment, the temptation to stretch maintenance windows is real. Production schedules push hard, and every hour of downtime shows up on a spreadsheet. But real-world conditions in food processing—humidity, washdown chemicals, fine organic dust, and constant temperature swings—don't care about optimistic spreadsheets. Pressing for realistic maintenance intervals means accepting that a gearbox exposed to daily high-pressure cleaning will not last as long as the same unit in a dry warehouse. It means building schedules around actual failure data from your own floor, not generic manufacturer estimates.
The conversation has to shift from “how long can we run this?” to “what does this specific line, in this specific room, with this specific product actually require?” That requires logging every unplanned stop, every worn seal, every bearing that gets noisy after six weeks instead of six months. Once you have that history, you can set intervals that prevent most breakdowns without over-maintaining. It also means involving the maintenance crew in planning—they know which pumps cavitate after CIP cycles and which conveyors need belt tension checks after a weekend shutdown. Their input turns a theoretical interval into a workable one.
Finally, realistic maintenance intervals are not a one-time fix. They need review every quarter, or after any significant line change. A new sauce with higher acidity might eat through gaskets faster. A faster filler might put more vibration into the frame. If you treat the maintenance calendar as a living document rather than a static policy, you stop fighting surprises. You schedule work when it is actually needed, keep food safety audits clean, and avoid the midnight call that starts with “the line is down and product is on the floor.”
Weigh the cost of lost production against the supplier’s support record
Every hour a machine sits idle because a critical part hasn’t arrived translates into real money—missed orders, overtime to catch up, and strained customer relationships. Before signing with a new supplier, pull up their actual response times and resolution history, not just the glossy case studies. A vendor with a modest price advantage but a track record of leaving you stranded for a week during peak season can erase years of savings in one breakdown.
Dig into how they handle urgent breakdowns: do they offer priority diagnostics, local spare parts inventory, or a dedicated escalation path? Suppliers who measure their own mean time to recovery and share that data openly tend to take downtime as seriously as you do. The real cost comparison isn’t between two invoices—it’s between one supplier that gets you running again in four hours and another that leaves you waiting for three shifts.
A supplier’s support record also shows up in less obvious ways—how quickly they answer technical questions, whether their engineers proactively flag wear patterns, or if they offer remote monitoring to catch issues before they stop production. Lost production isn’t just about the moment of failure; it’s the ripple effect of delayed maintenance and slow troubleshooting. Choose a partner whose support record proves they understand that every minute of downtime has a price tag.
FAQ
Look for ISO 8573-1 Class 0 certification for oil-free air, plus HACCP or FDA compliance if the compressor contacts food surfaces. Not all "oil-free" claims are equal, so verify test data.
Request third-party lab reports measuring oil content below 0.01 mg/m³. Ask for continuous oil monitoring options or inline sensors that alarm on contamination.
Choose suppliers offering easy-access filtration, stainless steel valves and fittings, and washdown-rated components. A modular design allows quick part swaps without specialized tools.
Yes, especially if your facility runs 24/7. A supplier with regional technicians and spare parts inventory can cut emergency response from days to hours.
Factor in energy consumption at your expected load, filter replacement intervals, and expected service life. A slightly higher upfront cost may pay back via lower kW per CFM.
Ask if the supplier provides integrated dryers, coalescing filters, and point-of-use filtration. Confirm the dew point meets your process and packaging requirements, usually -40°F or lower.
Generally no. Food grade requires oil-free compression elements, stainless piping, and special coatings. Retrofitting often voids warranties and fails audits.
Ask for case studies or references from similar facilities (bakeries, beverage plants, meat processing). Inquire about their understanding of specific risks like allergen cross-contact or moisture control.
Conclusion
For food processors, choosing an oil-free air compressor starts with nailing down exactly what certification or documentation your auditors will accept—"technically oil-free" and "Class 0" are not always interchangeable, and your vendor should be able to walk you through the specific ISO 8573-1 classifications you are expected to meet for each point of use. Instead of over-specifying clean air for the entire facility, map out where compressed air actually touches food, packaging, or production surfaces, and match purity levels to those contact points; this keeps capital and operating costs sensible without weakening compliance. Before shortlisting, request references from plants that run under similar conditions—whether that means wet washdowns, flour dust, cold storage, or high ambient heat—because a machine that performs well in a clean room may struggle in a bakery or poultry line.
The compressor itself is only part of the system: dryers, downstream filters, storage receivers, and condensate drains all influence whether the air stays food-grade by the time it reaches your process, so ask the supplier to specify the complete air-treatment train rather than just the airend. In a food environment, maintenance intervals pulled from a generic brochure rarely hold up—washdown chemicals, humidity, and fine organic dust can shorten seal and filter life, so push for service schedules based on actual operating conditions and documented failure rates. Beyond that, compare the supplier's local support record and typical emergency response time against the hourly cost of stopping your line; a low upfront quote means little if a down compressor can idle an entire packaging shift while you wait for parts or a technician.
Contact Us
Contact Person: Mia
Email: [email protected]
Tel/WhatsApp: +86 19821985894
Website: https://www.seize-air.com