Dual Channel Tissue Cutter Vendors: How to Choose the Right Supplier for Precision Cutting
2026-10-25
Choosing a dual channel tissue cutter vendor is rarely just about hardware specs. It’s about trusting that the supplier understands the fine line between a clean cut and a compromised sample. With precision on the line, the wrong choice can quietly erode your lab’s consistency—and your confidence. That’s why knowing what separates a dependable partner from a one-time seller matters. In this guide, we’ll walk through the practical factors that actually affect cutting accuracy and long-term reliability. And if you’re already weighing options, keep an eye on how DAXIN approaches these challenges—it might change the way you evaluate every vendor.
Why Blade Alignment Matters More Than Motor Power
A high-powered motor might sound impressive on paper, but it can't compensate for a cutting edge that isn't meeting the material at the correct angle. If blades are even slightly misaligned, they'll fight each other or the deck, wasting torque, heating up bearings, and leaving ragged cuts. Alignment determines how cleanly the edge slices; power only determines how fast you can spin a dull or crooked blade.
Think of it like a car with misaligned wheels. You can add more horsepower, but the tires will still scrub and wear unevenly, and the vehicle won't track straight. The same happens with blades: poor alignment creates vibration, uneven load, and premature wear on spindles and belts. A modest motor with perfectly trued blades will often outperform a large motor with blades that are fighting their geometry.
Before upgrading the power source, check the blade bar for flatness, spindle bolt torque, and runout. Many cutting problems that get blamed on a weak motor disappear once the alignment is corrected. In most cases, the real bottleneck isn't horsepower—it's geometry.
Decoding the Dual-Channel Advantage for Cleaner Cuts
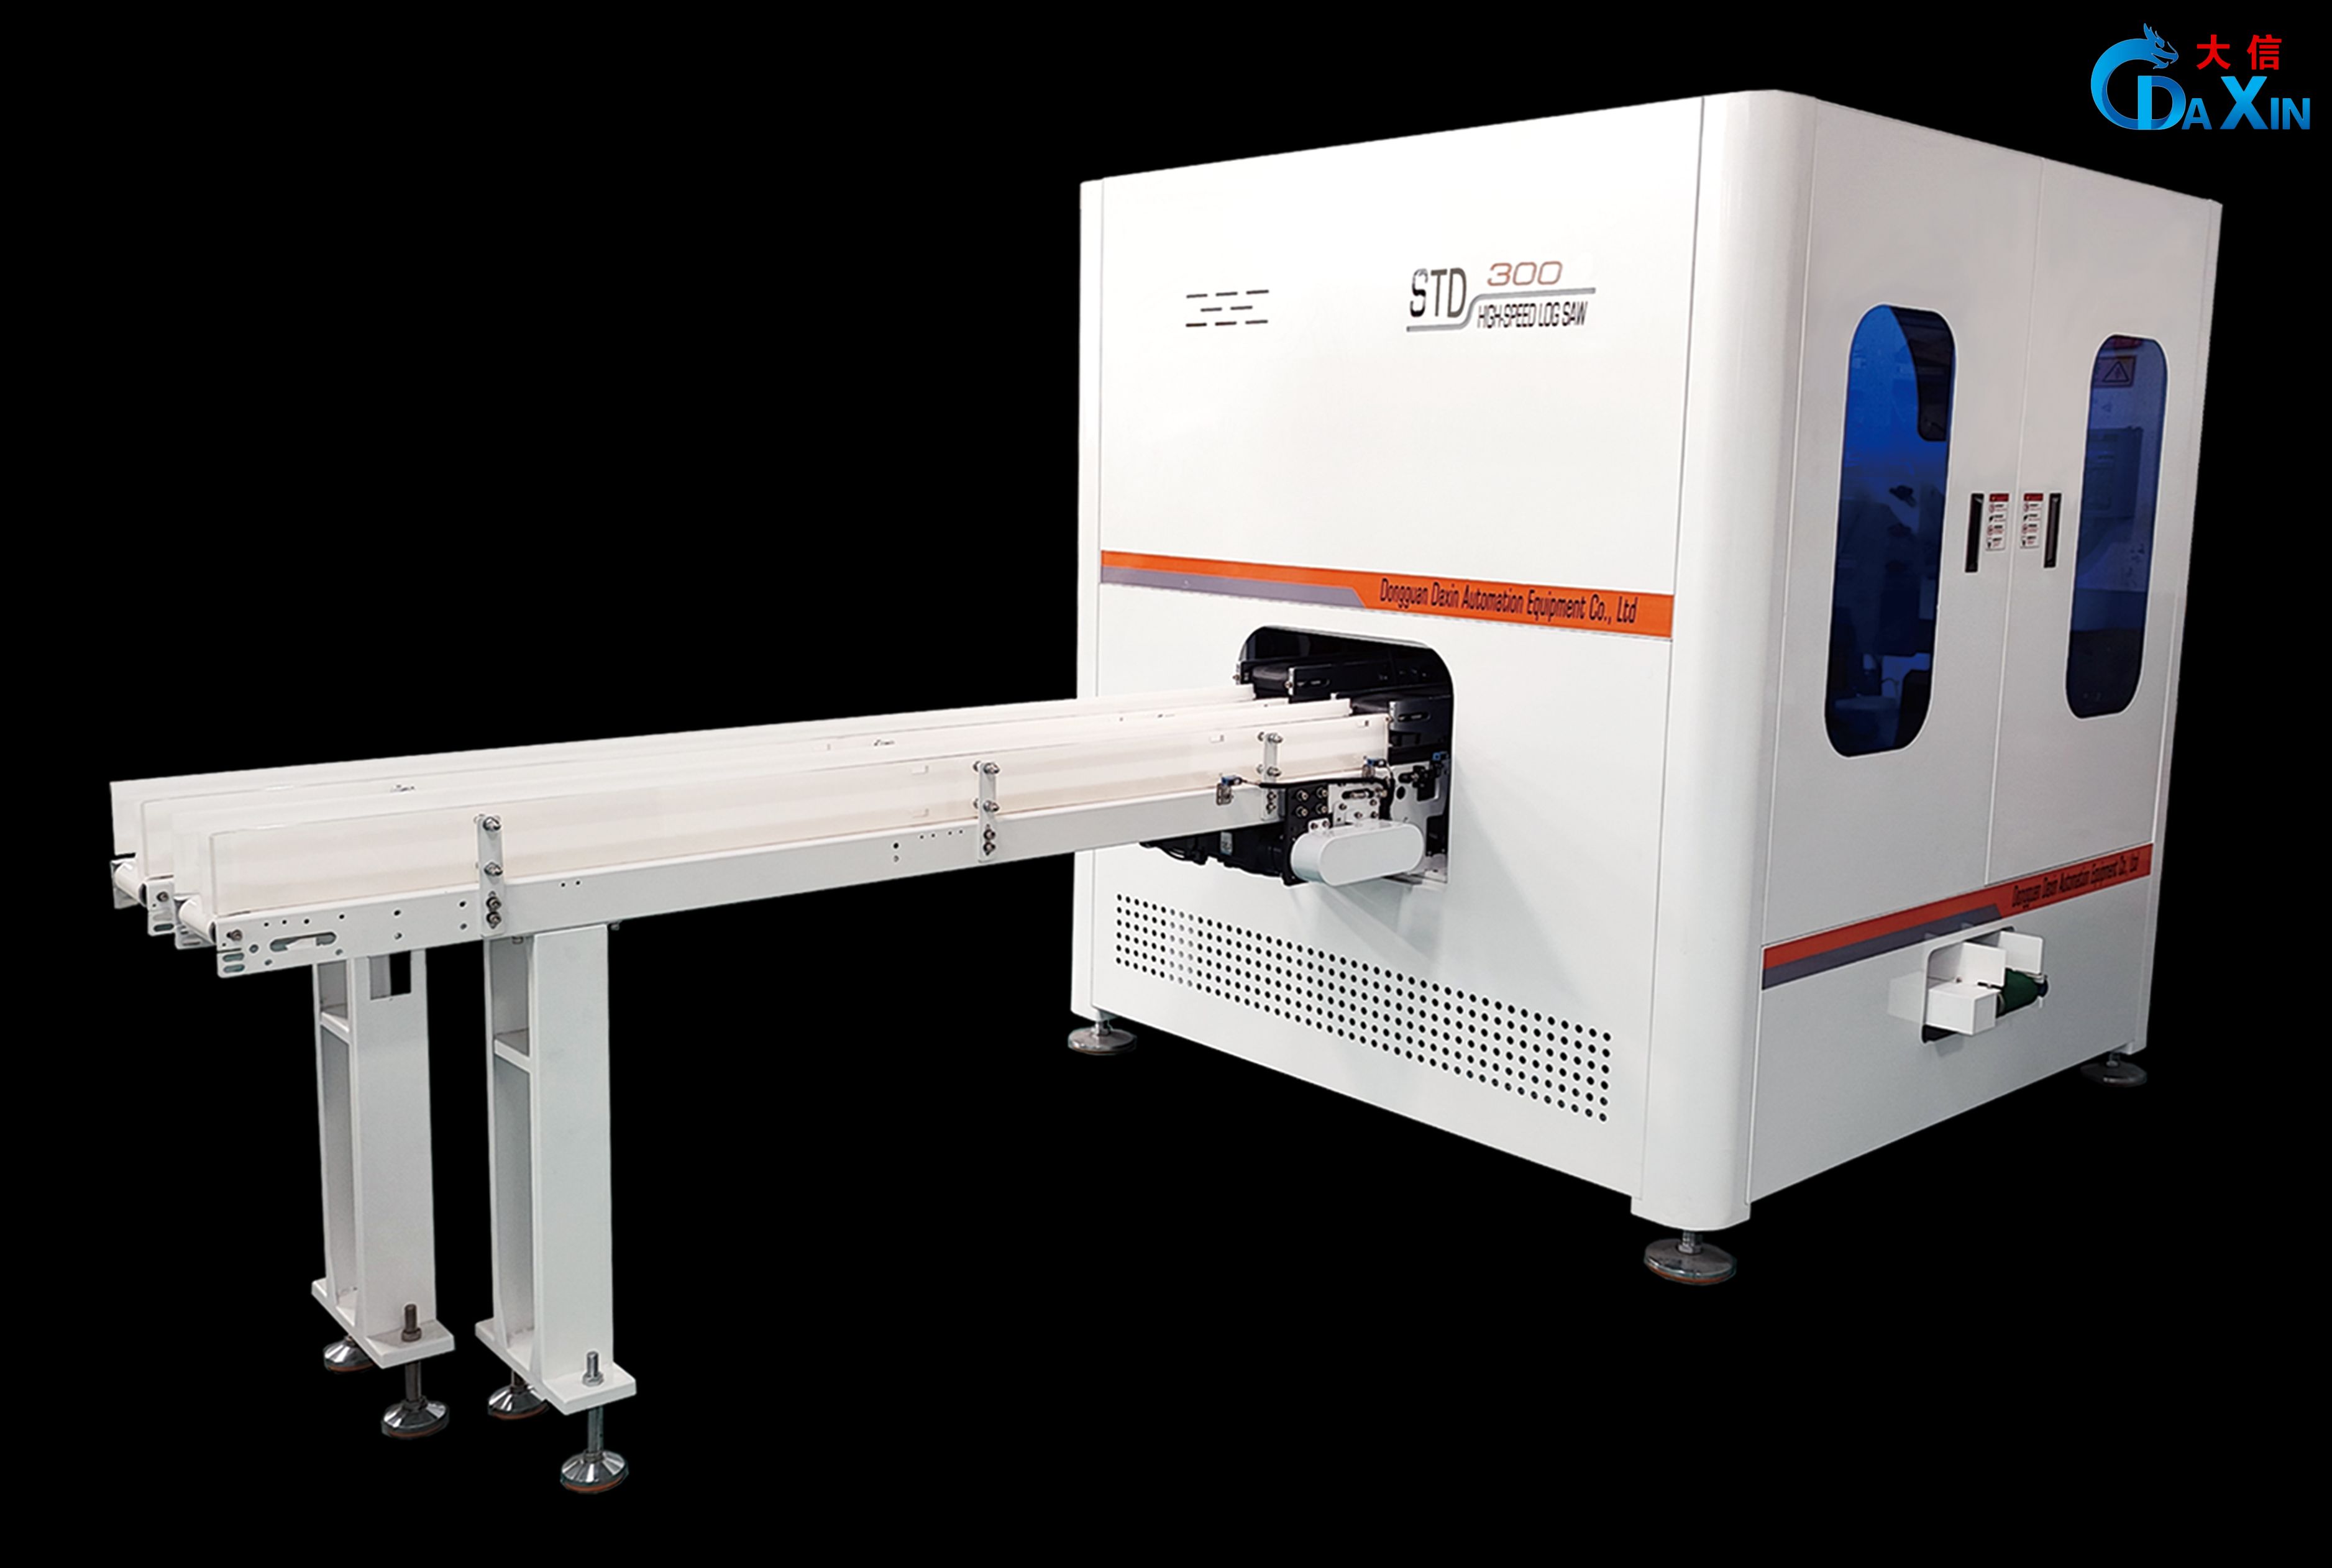
Most cutting tools force a single path to do everything—guide the blade, clear debris, and manage heat. That crowded workflow leads to microscopic tearing and rough edges. A dual-channel design splits these jobs into two dedicated lanes, so the blade never fights for space with waste removal or cooling. The result is a cut where the material separates exactly where you intend, not where friction and pressure say it should.
Think of the first channel as a stabilizer. It holds the material steady and directs airflow right at the contact point, preventing fibers from shifting mid-cut. The second channel handles the aftermath—pulling chips and dust away before they can wedge under the blade and cause jagged deviations. By giving each task its own route, the tool eliminates the bounce and grab that typically leave a fuzzy, uneven line.
On the workbench, this means less sanding, fewer passes with a deburring tool, and a finished edge that feels almost polished straight off the machine. Whether you are slicing through plywood, acrylic, or thin metal, the dual-channel approach keeps the cut path clean and predictable. It is not just about sharper blades—it is about giving the blade room to do its one job without interference.
Vendor Claims vs. Actual Cutting Tolerances
Most data sheets list tolerances measured on fresh consumables, flat sheet stock, and a temperature-controlled table. The moment you move to a production floor, those numbers tend to drift. A plasma system might be quoted at ±0.5 mm, but cutting 20 mm plate with slightly worn nozzles or inconsistent air pressure can easily push real variation past ±1.2 mm.
The gap often comes down to unstated variables. Vendors rarely highlight how material stress, heat buildup along a long cut path, or even the way a plate is clamped will change kerf width and edge squareness. Instead of accepting a single printed figure, ask for a trial cut on your own stock and measure the critical features with a calibrated gauge.
Measurement conventions also create confusion. Some suppliers quote average kerf width rather than dimensional accuracy, or they test only straight cuts while ignoring hole diameter, corner radius, and bevel angle. A fair comparison requires defining the tolerance zone, the inspection method, and whether the stated number holds across a full production run, not just a demo piece.
Material Compatibility Tests You Can Run in a Day
A practical way to check material compatibility without waiting weeks is to run a short immersion study. Cut small coupons from the plastic, elastomer, or coated metal you're evaluating, then submerge them in the process fluid or cleaning agent at the maximum expected temperature. Leave one set at room temperature and another in a sealed jar placed in a warm water bath or lab oven. After eight to twelve hours, pull the samples, blot them dry, and look for swelling, softening, discoloration, or surface tack. Record weight and thickness before and after exposure—changes beyond a few percent typically signal trouble.
If the fluid is aggressive or the application involves intermittent contact, a repeated dip-and-dry cycle works better than static soaking. Use a simple timer to alternate ten minutes immersed and fifty minutes drying, and run six to ten cycles while checking dimensional stability and hardness with a durometer if you have one. Some rubbers pass a single soak but fail after repeated wet-dry swings because plasticizer leaches out or microcracks open. For adhesives or sealants, apply a thin film to the substrate, let it cure fully, then place a drop of the test chemical on the surface under a watch glass. Lift the glass after a few hours and probe the film with a wooden pick for softening or loss of adhesion.
Don't overlook stress. A material that stays intact while unstressed may craze or crack when clamped in a slight bend or under a constant load. Bend a few strips over a mandrel or clamp them in a fixture before exposure, then check for cracks with a magnifier. Document everything with phone photos against a neutral background, and note the fluid batch, temperature, and exposure time on the image or in a simple log. These same-day tests won't replace long-term qualification, but they catch obvious mismatches early and give you a solid shortlist before committing to more expensive trials.
The Real Cost of Downtime With Generic Suppliers
当一台关键设备因劣质替换零件而停机时,会计部门看到的只是维修费用和几小时的生产损失。但真实成本远不止这些:产线工人闲置、交货承诺被打破、客户开始怀疑你的可靠性。有个中型食品加工厂曾因为一个便宜的传送带轴承故障,导致整条包装线停摆了六个小时,最终不仅支付了双倍的紧急维修费,还错过了一整车发往连锁超市的货。
更隐蔽的是,通用供应商往往缺乏针对你具体工况的备件适配数据。你不得不在停机后反复沟通规格、等待对方查库存、再安排最快次日达的物流。每一次拖延都让损失成倍增加。相比之下,专业供应商会提前分析你的设备运行参数,把易损件提前备在本地仓,并在故障发生前给出更换预警。这不是简单的买卖关系,而是把停机风险从你身上转移到了供应商身上。
一项针对中型制造企业的跟踪调查显示,仅包装和装配环节,平均每年因非原厂或非定制零件造成的意外停机达到11小时,折算下来接近全年产能的0.4%。这还不包括赶工产生的加班费、空运补货费用,以及客户因延迟交付而要求的折扣。通用供应商的低单价,往往就是在这些看不见的地方被加倍讨了回去。
Building a Supplier Checklist That Survives Production Pressure
Every production floor has a rhythm, and any supplier checklist that ignores that rhythm gets shredded by the second shift. Start by mapping each checklist item to a moment on the line where it actually gets used—incoming inspection, pre-kit staging, final assembly—not to a conference room ideal. If a step can't be executed by someone wearing gloves and holding a torque wrench, it doesn't belong on the list. Real survival means writing checks that fit into hands already busy, not adding paperwork that gets forged after the fact.
Pressure turns shortcuts into habits, so the checklist needs to make the right shortcut obvious. Instead of ten vague words like "verify material," use one line that points to a specific marking, a go/no-go gauge location, or a shelf-life label format. When the line stops and everyone is watching, a good checklist reads like a single decision: pass or quarantine. If an item requires interpretation, it fails at exactly the moment you need it most. The strongest lists are written by people who have been blamed for a line-down, because they know which details actually stop a defect versus which ones just stop a signature.
Finally, treat the checklist as a living mechanism, not a laminated poster. After every major production surge or material change, walk the line with the actual sheet in hand and cross out or rewrite any line that didn't catch a real issue. If a supplier pushes back on a new requirement, ask them to demonstrate how their current process already meets the intent—then adjust the wording to match that working method. A checklist survives production pressure by earning trust through repeated, boring victories, not by being enforced harder.
FAQ
Dual channel cutters let you run two independently controlled sections at once, which matters when you're juggling biopsies from different blocks or need exact parallel sections for staining panels. Look for machines where the channels share a stable baseplate but don't force you to swap blades between runs—otherwise you lose the time benefit.
More than the motor spec sheet suggests. A vendor may offer a fast feed rate, but if their blade holding system has runout or requires frequent recalibration, you'll spend more time on maintenance than cutting. Ask for a trial run with your own tissue types—especially dense or fatty samples—and measure section thickness consistency from both channels simultaneously.
Yes—if a supplier can't explain how the two channels stay synchronized under load, or if they claim zero variation without test data, treat that as a warning. Also be wary of suppliers who only demo on paraffin blocks and refuse to test frozen or calcified tissue. A good vendor will want to see your hardest samples, not hide from them.
Request the average response time for on-site repairs in your region, and whether they stock replacement parts locally or ship from overseas. For dual channel models, ask how they handle calibration after a blade change—some machines need a technician visit, while others have self-aligning channels that only need a quick software check. The latter saves days of downtime.
Not always. Precision depends on the guide rail system, anti-vibration mounts, and how the stage handles micro-stepping. Mid-range suppliers sometimes use the same linear guides as premium brands but charge less because they skip touchscreen extras. Focus on measured section thickness variance across both channels over an 8-hour shift, not the price alone.
Ask them to cut a series of ribbons from a homogeneous tissue block on both channels at the same time, then measure the ribbon thickness under a microscope or with a micrometer. Better yet, send them three blocks of your own—one normal, one dense, one with hard inclusions—and compare the sections side by side. If they hesitate to ship samples back, that's your answer.
Software should let you store cutting protocols per tissue type and apply them to both channels independently, but it shouldn't be the main selling point. Many labs overpay for fancy interfaces while the mechanical parts are mediocre. Check whether the software logs cutting force and section count—that data helps you predict blade wear before it ruins a batch.
Yes, but only if the training covers troubleshooting common dual-channel issues, like feed rate mismatch between channels or ribbon splitting. Generic 'how to press start' sessions are useless. Ask if the trainer has worked in a histology lab, not just sold machines, and request a follow-up session after your team has used the cutter for a month.
Conclusion
When evaluating dual channel tissue cutter vendors, buyers often fixate on motor wattage, yet blade alignment has a far greater influence on edge quality. A perfectly paired blade set glides through layered tissue without tearing, while a misaligned unit—even one with extra power—produces ragged margins that downstream processes cannot fix. The dual-channel design itself matters only if both channels share the same axial plane; otherwise, you get uneven compression and wasted material. Vendor spec sheets rarely reveal this. Ask for a live cutting demo on your own substrate, and measure the actual kerf and burr height rather than trusting a polished brochure. A half-day test with three material grades will tell you more than a year of marketing claims.
The hidden expense of choosing a generic supplier shows up as unplanned stoppages, blade swaps, and rejected lots. Downtime costs compound quickly when a cutter drifts out of tolerance mid-batch. Build a checklist that forces vendors to prove repeatability: request a documented run of 500 consecutive cuts, check temperature rise after 30 minutes, and confirm replacement blade lead times. If a supplier hesitates on any of these, walk away. The right partner treats alignment verification as routine, not as a premium service. Precision cutting is not about a single impressive demo—it is about whether the machine and the vendor both hold tolerance when production pressure peaks.
Contact Us
Contact Person: Sam Xie
Email: [email protected]
Tel/WhatsApp: 86-18938538530
Website: https://www.daxin321.com/