China 132kV Galvanized Angle Steel Transmission Tower Supplier for Durable High-Voltage Infrastructure
2026-09-23
Every year, utilities lose millions to transmission tower failures caused by subpar steel or rushed galvanizing. Yet procurement teams still chase the lowest bid—until a 132kV line goes dark. Anbang, a China-based supplier of galvanized angle steel transmission towers, takes a different approach: designing for 50-year service life in corrosive and high-wind zones. In this article, we break down what actually makes a 132kV tower infrastructure durable—and why Anbang's engineering choices are gaining ground among global EPC contractors.
Galvanized Angle Steel: Still the Smart Choice for 132kV Lines
When planning a 132kV transmission line, the conversation inevitably turns to materials that can handle decades of wind, ice, and corrosion without demanding constant attention. Galvanized angle steel keeps earning its place on the pole structure drawings—not because it's the only option, but because it quietly outperforms alternatives in the field. The hot-dip coating bonds to the steel at a metallurgical level, creating a barrier that shrugs off moisture and salt spray far longer than paint or weathering steel ever could in coastal or industrial corridors. For line owners who'd rather spend on capacity upgrades than repainting crews, that longevity is impossible to ignore.
Beyond corrosion resistance, angle steel brings a level of adaptability that newer composite or tubular designs often lack. Standard leg sizes and bolt-hole patterns mean a damaged member can be replaced with a stock piece from a local yard—no custom fabrication lead times, no specialized connectors. In remote stretches where a 132kV line might run fifty kilometers from the nearest depot, that logistical simplicity translates directly into shorter outage windows. Field crews know the material; their tools fit it; and the erect-and-forget nature of a well-galvanized lattice tower removes one more variable from an already demanding construction schedule.
Cost comparisons tend to focus on initial purchase price, but the smarter math accounts for a forty-year service life. Galvanized angle steel towers often weigh less than equivalent concrete or tubular steel structures, cutting foundation requirements and crane time without sacrificing stiffness under galloping conductor loads. When you factor in the salvage value of the steel at decommissioning—something composites simply don't offer—the lifecycle economics remain compelling. For 132kV lines that must balance reliability with tight capital budgets, the choice isn't about nostalgia for lattice towers; it's about letting proven engineering do the heavy lifting.
What Hot-Dip Zinc Does That Paint Can't
Hot-dip zinc forms a metallurgical bond with steel, becoming part of the surface rather than sitting on top of it. Paint simply adheres mechanically, and once scratched or chipped, the underlying metal is exposed to corrosion. Zinc, in contrast, sacrifices itself slowly and predictably, sealing off edges and corners that paint struggles to cover.
In harsh environments like marine or industrial settings, galvanized steel shrugs off moisture and salt that would quickly creep under a painted coating. The zinc layer corrodes preferentially, protecting the steel even at cut ends or small imperfections. No paint system offers this built-in self-healing behavior without constant inspection and touch-up.
Maintenance cycles tell the story: a properly galvanized structure can last decades without attention, while painted steel demands regular repainting once the film breaks down. The initial cost difference disappears when you factor in access equipment, surface preparation, and downtime for repainting. Hot-dip zinc simply does what paint cannot—it stays put and keeps working.
Shop Floor Checks That Separate Reliable Towers from the Rest
A tower that passes the final once-over but leaves the shop with a thin spot in the basin or a fan hub that was never dynamically balanced is a warranty claim waiting to happen. The shops worth trusting run checks on the floor, not just on paper: they measure wall thickness at the low points where corrosion starts, inspect every structural weld for undercut and porosity, and spin each fan assembly before it's mated to the gearbox. If a vendor can't show you those records with time stamps and the operator's initials, walk away.
The difference shows up in small things. On a truly reliable tower, the drift eliminators seat flush against the supports, the access door gaskets aren't stretched or nicked during assembly, and the basin doesn't flex when you push on the sidewall. Cheaper shops skip the dry-fit step and hope the field crew will fix misaligned braces or shim the motor base later. By then the tower is already on a truck, and the owner pays for every shortcut in extra rigging hours and early component wear.
Ask where the line pressure test happens and how many cycles the float valve gets before shipping. Good shops will fill the cold water basin, mark the waterline, and let it sit overnight to catch pinhole leaks that a quick visual pass will miss. They'll also run the drive train at full speed for at least an hour with the access doors on, because that's when misaligned couplings and resonant panels show up. These aren't exotic tests; they're just the ones that separate factories that stand behind their towers from those that only sell a set of drawings.
Why Lattice Geometry Still Wins for High-Voltage Spans
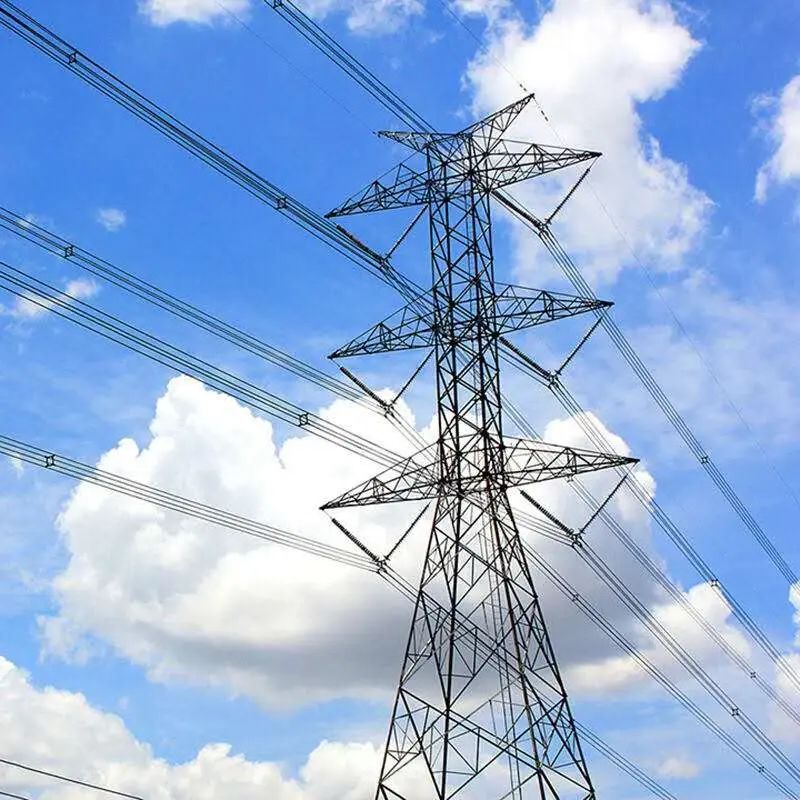
Lattice towers carry high-voltage conductors across long distances because the open framework routes tension and compression along clearly defined paths. A single solid pole must resist bending as a monolithic beam, which puts the entire cross-section to work inefficiently. In a lattice mast, diagonal bracing splits the wind and cable loads into a series of push-pull forces. This lets designers use thinner, lighter angle sections where they matter, rather than thickening a whole cylinder to survive the worst-case gust at one height.
The triangular arrangement that shows up again and again in lattice legs and crossarms isn't a stylistic leftover. It prevents the structural joints from acting like hinges under twisting loads. On long river crossings or mountain ridges, the tower sees not just transverse wind but also uneven ice buildup and conductor galloping. A lattice frame handles these off-axis forces without building up fatigue-prone welds as quickly as a smooth tubular design, mainly because the bolted connections allow micro-slippage that sheds peak stress.
Field assembly also favors the lattice. The pieces can be hot-dip galvanized in compact batches, bundled flat, and carried by mule or helicopter into terrain where a pre-welded monopole would never fit. Once the tower is up, a visual inspection of each member is straightforward—cracked or corroded angles are replaced individually, without taking the line out of service for a full structural teardown. That incremental repairability, combined with lower steel mass per kilometer, keeps the initial cost and the fifty-year maintenance story on the side of the lattice.
Moving 30-Meter Steel Structures Across Oceans Without Damage
The logistics of shipping a 30-meter steel structure start long before it reaches the dock. Engineers map the center of gravity, weld temporary lifting lugs and stiffeners, then use self-propelled modular transporters to creep the load onto a heavy-lift vessel. Every inch of the route is surveyed for bridge clearances, ground bearing pressure, and turning radii. At the quay, the structure is placed on custom steel grillage that spreads the weight across the vessel deck, preventing point loads that could crack welds or deform frames during the voyage.
Once at sea, the real challenge is motion. A 30-meter steel assembly can flex and twist as the ship rolls and pitches. Sea fastenings—chains, turnbuckles, and welded stoppers—are tensioned in a calculated pattern that allows the cargo to breathe with the ship while still holding it against sliding and tipping. Voyage data recorders and accelerometers feed readings back to the bridge, and if a storm builds, the master may alter course or slow down to keep accelerations below the threshold that would fatigue the steel.
Arrival is just as delicate. The same grillage system is unbolted or cut away after the ship is stable alongside the discharge berth. Jacking towers or strand jacks may lift the structure enough to slide SPMTs underneath, then the load rolls off in reverse of how it came aboard. A final dimensional survey checks for any permanent deformation before handover, wrapping up a move that demanded precision on land and patience at sea.
The Real Lifespan of a Transmission Tower in Corrosive Air
A transmission tower designed for a 50-year service life rarely sees that full span when it stands within a few kilometers of an industrial zone or a salt-laden coastline. The steel members and fasteners start losing zinc from their galvanized coating within the first decade, and once the underlying carbon steel is exposed, rust spreads quickly through the lattice joints where moisture and chlorides collect. What engineers call "corrosive air" is not a single threat but a cocktail of sulfur dioxide, chloride aerosols, and humidity cycles that eat away at the metal at rates far beyond inland assumptions.
Field inspections in coastal and heavy-pollution corridors consistently show tower legs and gusset plates reaching critical section loss in 20 to 30 years, sometimes less if the tower was built with older galvanizing methods or if birds and dust have built up corrosive nests. The real lifespan, therefore, hinges less on the original design calculations and more on the upkeep: recoating intervals, replacement of bolted connections, and whether the owner budgets for drone-based or climbing inspections every three to five years. A tower that is ignored can fail structurally while the line still looks intact from the ground.
There is no single "real lifespan" that applies everywhere, because local microclimates matter enormously. A tower 500 meters inland from the shore may last twice as long as one right at the tideline, and a tower downwind of a coal-fired plant may need major rehabilitation before its 25th birthday. What holds true across cases is that corrosive air compresses the maintenance clock: small touch-ups delayed by a year become full member replacements delayed by a decade, and eventually the economics of rebuilding overtake the economics of repair.
FAQ
It combines a high strength-to-weight ratio with excellent corrosion resistance, so the towers remain stable for decades without frequent repainting or section replacement.
Yes, most Chinese suppliers accept site-specific load calculations and soil data, then modify member sizes, bracing patterns, and bolt connections to match the requirements.
For a standard 132kV angle steel tower set, expect around 30 to 45 days, though complex custom configurations or larger orders may push that closer to 60 days.
Reputable manufacturers can work with IEC, ASTM, or specific national grid standards, but you need to clearly state which code applies before production begins.
They are shipped as bolt-together segments rather than one welded piece, which lowers freight costs and allows rapid on-site assembly using standard hand tools.
The galvanized coating typically protects steel for 25 to 30 years in normal outdoor environments, so maintenance is mostly limited to occasional bolt torque checks and clearing nearby vegetation.
Many suppliers can offer preliminary foundation recommendations based on the tower reactions and soil report, but final civil drawings are usually handled by a local engineer familiar with site conditions.
Conclusion
For utilities planning 132kV transmission links, a dependable Chinese angle steel tower supplier still leans on galvanized lattice construction for good reason. Hot-dip zinc does more than coat the surface: it forms an abrasion-resistant metallurgical layer that keeps protecting exposed edges and minor scratches in a way field-applied paint simply cannot. The geometry matters as well. Bolted lattice frames shed wind load efficiently, reduce steel weight per kilometre, and allow individual members to be inspected or replaced without dismantling an entire structure. On the factory floor, the difference between a tower that lasts and one that surprises you later usually comes down to unglamorous checks: raw angle straightness, hole alignment after punching, weld penetration, and zinc thickness measured at the thinnest point rather than an average.
Shipping 30-metre steel structures across oceans without damage also depends on modular design. Sections are typically trial-assembled, match-marked, then broken down into stackable bundles with protected flange faces and sling points. Once erected in coastal or industrial corridors, the real lifespan often hinges on small details—avoiding water traps at joints, using sealed interfaces, and matching bolt coatings to the galvanized members. In practice, well-built galvanized angle steel towers in moderately corrosive air commonly remain serviceable for five decades or more with only routine bolt-tension checks, which is why careful buyers look beyond price and ask for batch traceability, salt-spray test data, and a shop that can explain how it controls distortion during welding.
Contact Us
Contact Person: antor khan
Email: [email protected]
Tel/WhatsApp: 8613863903569
Website: https://www.qdabtower.com/